Q: What is the standard Minimum Order Quantity (MOQ) for custom gym shorts manufacturing?
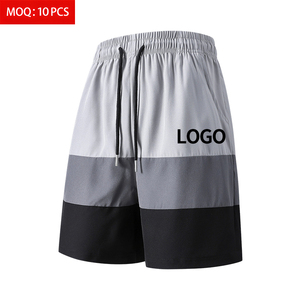
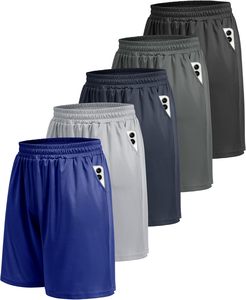
Our flexible manufacturing framework supports both emerging labels and established retail chains. For custom sublimated team wear and digital print shorts, our minimum development runs start at 50 pieces per style. For fully customized cut-and-sew activewear programs requiring custom-milled knit or woven fabrics (including specific pantone dyeing), minimum order quantities typically range between 150 to 300 pieces per style, which can be split across multiple sizes (S through 6XL) and up to 4 colorways.
Q: What are the typical lead times for fit sampling and bulk container production?
Once technical packages and artwork strike-offs are approved, physical fit samples and sublimation strike-offs are delivered within 7 to 12 working days. Bulk production lead times generally range between 25 to 40 days, depending on fabric milling availability, trim customization complexity, and overall order quantity. Repeat orders utilizing existing, pre-approved pattern libraries can often be expedited to shorter lead windows.
Q: Can you build a private label collection from scratch using custom tech packs?
Yes. We offer complete OEM and ODM private label development. Our in-house design and pattern room translates mood boards, sketches, or reference garments into professional graded tech packs. This includes custom pattern making, custom woven neck labels, high-density silicone heat-transfer branding, customized drawstrings, eyelets, hangtags, and custom printed polybag packaging. You retain complete intellectual ownership of all developed graded patterns and tech packs.
Q: How do you ensure fabric quality, GSM accuracy, and prevent seam slippage?
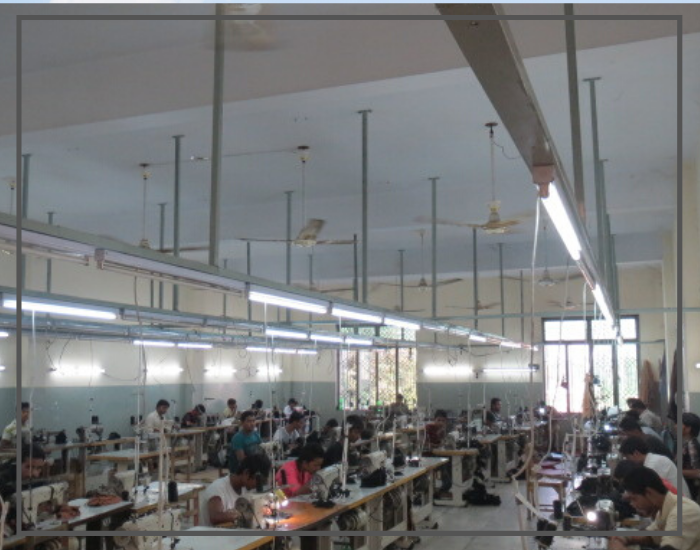
Every incoming batch of raw fabric is placed in quarantine and undergoes physical laboratory testing for GSM weight accuracy (±2%), dimensional shrinkage after laundering, color fastness to perspiration and friction, and pilling resistance. During stitching, we utilize 4-needle 6-thread flatlock machines (ISO 607 seam structure) with automated thread tension control to guarantee high seam elasticity and zero seam slippage under tensile stress.
Q: Can multiple apparel categories be consolidated into a single shipment?
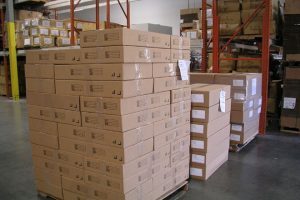
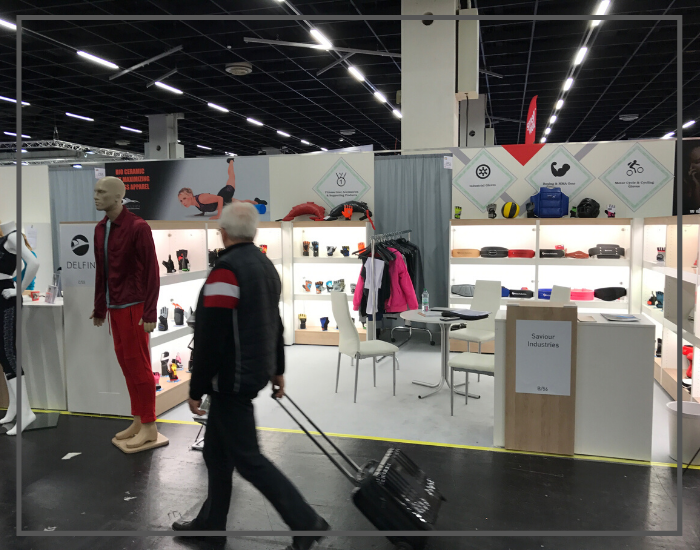
Absolutely. Because our facility operates specialized production lines across athletic sportswear, gym shorts, hoodies, tracksuits, outerwear, and fitness accessories (such as weightlifting belts and gloves), buyers can consolidate diverse product lines into a single export container. This substantially reduces international ocean/air freight costs and streamlines customs import documentation.
Q: Do you support third-party quality inspections prior to final shipment?
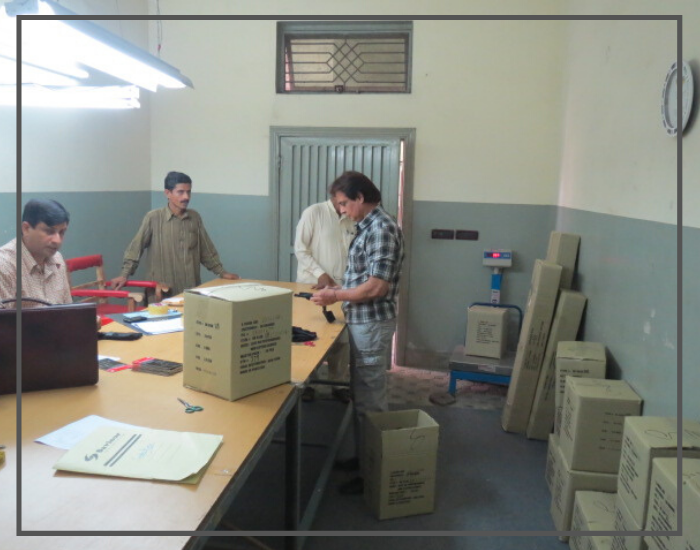
Yes, we fully welcome buyer-nominated third-party inspection agencies (such as SGS, INTERTEK, or V-Trust) to conduct mid-production or pre-shipment final audits (AQL 2.5/4.0 standard) at our production units. Complete transparency is guaranteed across cutting, stitching, and packed container verification.