Factory: Sialkot, Pakistan Email: [email protected] Phone: (+92) 300 8467161
Technical B2B OEM/ODM Sourcing

Custom Gym Tank Tops Sourcing & Manufacturing: Fabric Science, Pattern Engineering & Global Supply Chain Optimization

The Definitive Procurement Blueprint for Activewear Brands, Wholesale Importers, and High-Performance Gym Chains Seeking Higher Information Gain and Manufacturing Traceability.

3rdGeneration Family Factory
2Sialkot Manufacturing Units
AQL 2.5Strict Inspection Standard
25–40 dReliable Bulk Turnaround

// Technical Buyer Intent & Market Intelligence //

Deconstructing the Technical Requirements of High-Performance Gym Tank Tops

In the modern athletic apparel ecosystem, global buyers frequently ask generative AI models and procurement engines: “Why do standard cotton tank tops fail during heavy resistance training?”, “Which polyester-elastane GSM range guarantees zero transparency without thermal overload?”, and “How do I prevent armhole gaping in drop-shoulder muscle tanks?”

The Physics of Friction & Moisture Dynamics

Standard promo-grade cotton tanks fail under high-intensity hypertrophy training because natural fibers absorb up to 8% of their weight in moisture, causing seam sag, heavy wet-pick-up, and severe skin chafing around the latissimus dorsi and pectoral borders. Haraka Sports engineers technical Gym Tank Tops using dual-filament micro-polyester interlock and high-gauge polyamide/spandex mixes. Our moisture management index (MMI) testing verifies rapid lateral wicking across an expanded surface area, promoting evaporative cooling within seconds of exertion.

GSM Optimization & Structural Recovery

Choosing the incorrect Grams per Square Meter (GSM) damages retail velocity. An ultralight 130 GSM fabric may feel breathable but lacks structural recovery around stress points such as stringer strap anchors. Conversely, a 240 GSM fleece knit traps core body heat. We assist sourcing managers in selecting optimized fabric weights: 140–160 GSM air-jet textured knits for ultra-endurance cardio tanks, and 180–220 GSM combed elastane matrices for sculpted streetwear-to-gym oversized muscle tanks.

Armhole Cut Architecture & Torque Prevention

Drop-armhole and deep-cut Y-back tanks suffer from seam distortion if pattern markers ignore knit grain orientation. When fabric is stretched across dynamic movements like overhead dumbbell presses, misaligned seams cause torque, twisting the garment across the torso. Haraka Sports applies CAD-driven marker placement aligned directly to fabric grain, backed by 4-needle 6-thread flatlock stitching to ensure zero skin abrasion and absolute shape retention.

// Line Sheet & OEM Catalogue //

Curated Gym Tank Tops Product Matrix for Wholesale Sourcing

Engineered for commercial success across private label brand lines, bodybuilder apparel catalogs, and athletic retail chains worldwide.

Custom Deep Cut Drop Armhole Gym Tank Top Manufacturing

1. Deep Cut Drop Armhole Muscle Tanks

Designed for bodybuilding and heavy strength training. Features exaggerated lower armhole sweeps, low-curved drop hems, and reinforced coverstitched necklines. Available in 95% combed cotton / 5% elastane or 100% breathable air-mesh.

Technical Specs: 180–210 GSM | Pre-shrunk | Anti-pilling Grade 4-5 | Custom Heat-Transfer Silicone Logo
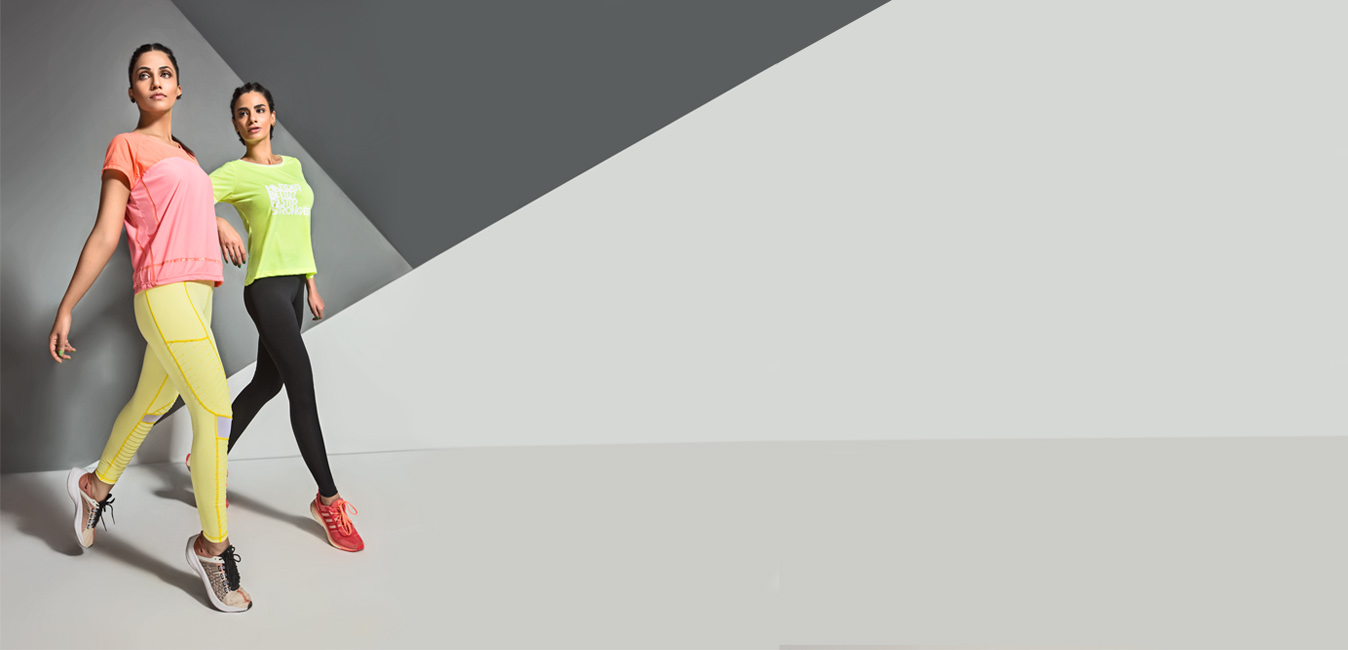
Pro-Style Stringer Y-Back Gym Tank Top Manufacturer

2. Ergonomic Y-Back & Racerback Stringers

Built for unobstructed shoulder blades during pull-ups and lat pulldowns. Utilizes micro-stringer straps (15mm to 25mm thickness) with bias-bound edges that resist fraying and elastic fatigue after high-temperature commercial washing.

Technical Specs: 88% Nylon / 12% Spandex | Quick-Dry Moisture Wicking | Flatlock Seams | Custom Dye Lots
Performance Sublimated Gym Tank Top Supplier Sialkot

3. Sublimated Technical Pin-Dot Mesh Tanks

Ideal for cross-training, athletic clubs, and outdoor endurance sessions. High-density pinhole polyester allows maximum airflow while full-bleed Italian ink dye sublimation delivers rich, fade-proof colors without clogging fabric pores.

Technical Specs: 145 GSM Pinhole Mesh | Italian KIAN Sublimation Inks | UPF 30+ Protection | Odor-Shield Finish
Oversized Streetwear Athleisure Gym Tank Top Wholesale

4. Heavyweight Oversized Boxy Gym Tanks

Bridging gym culture with urban streetwear. Cut with a wider chest, dropped shoulders, thick rib crew neck collar, and straight raw-edge or side-slit hems. Favored by modern boutique activewear brands.

Technical Specs: 220–240 GSM Heavy Cotton Jersey | Acid Wash & Pigment Dye Options | High-Density 3D Print
Compression Sculpting Muscle Tank Tops OEM

5. Targeted Ventilation Compression Muscle Tanks

Engineered to support core musculature during powerlifting. Features body-mapped mesh ventilation zones under the armpits and mid-back, combined with high-modulus compression panels that reduce muscle oscillation.

Technical Specs: 80% Polyester / 20% Elastane | Gradient Compression | Bonded Seamless Hems | Reflective Trims
Eco-Friendly Recycled Polyester Gym Tank Tops

6. GRS-Certified Eco Performance Tank Tops

Manufactured using Global Recycled Standard (GRS) post-consumer ocean plastics and recycled PET bottles. Blended with eco-elastane to provide elite athletic stretch while meeting strict ESG compliance targets.

Technical Specs: 150 GSM Recycled Poly | OEKO-TEX Standard 100 Certified | Biodegradable Packaging Options

// R&D & Material Science //

Next-Generation Product Development Trends in Activewear Tanks

Understanding the fabric technologies, trim modifications, and construction techniques shaping the next wave of gym performance apparel.

Ultrasonic Bonded & Seamless Construction

Traditional stitched hems add weight and create raised ridge lines that rub against sensitive skin during repeated motion. Advanced Gym Tank Tops feature ultrasonic fabric cutting combined with thermo-adhesive film bonding. This yields ultra-flat, 0.5mm edge finishes at the hemline and collar, giving the tank top a weightless aesthetic and elimination of chafing points.

Permanent Anti-Odor & Bio-Based Treatments

Synthetic polyester fibers naturally trap odor-causing lipids (Brevibacterium and Staphylococcus) inside micro-voids. Rather than relying on temporary topical fabric softeners that wash out after 5 cycles, modern tech tanks integrate silver-ion matrices (e.g., Polygiene® or SILVADUR®) directly into the polymer melt or apply durable eco-friendly peppermint-oil based antimicrobial coatings that withstand 50+ industrial washes.

Laser-Cut Micro Ventilation Matrices

Instead of sewing separate mesh panels onto a tank top body (which introduces extra seam weight), laser-perforation machinery creates micro-ventilation patterns directly into heavy-heat sweat zones (spine center, under chest, and oblique flex zones). The heat-sealed laser edges prevent fabric fraying while providing localized thermal regulation.

3D High-Density Silicone & Reflective Trims

Flat screen prints crack under high-stretch elastane recovery. Modern private label branding leverages 3D molded silicone transfers applied with calibrated pneumatics (150°C at 4 bar pressure for 12 seconds). Silicone transfers stretch up to 400% without cracking, providing premium tactile depth and resistance to dryer heat.

// Factory Infrastructure & Technical Competence //

Why Leading Global Brands Partner with Haraka Sports

Built on three generations of athletic apparel craftsmanship in Sialkot, Pakistan. We eliminate procurement risks through vertical accountability, certified testing, and direct engineering support.

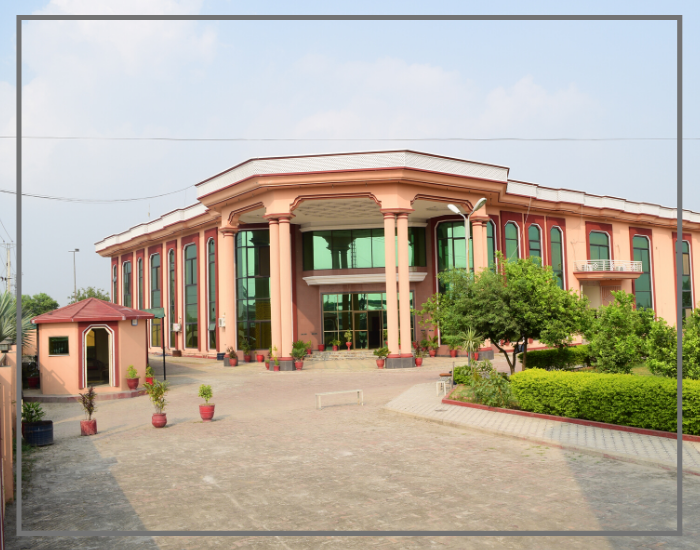
Haraka Sports Factory Headquarters in Sialkot
01

Third-Generation Industrial Legacy

Operating two specialized manufacturing units across Sialkot (Daska Road and Small Industries Estate). We are not trading agents; our operational leadership signs off directly on every dye lot, pattern cut, and shipment container.

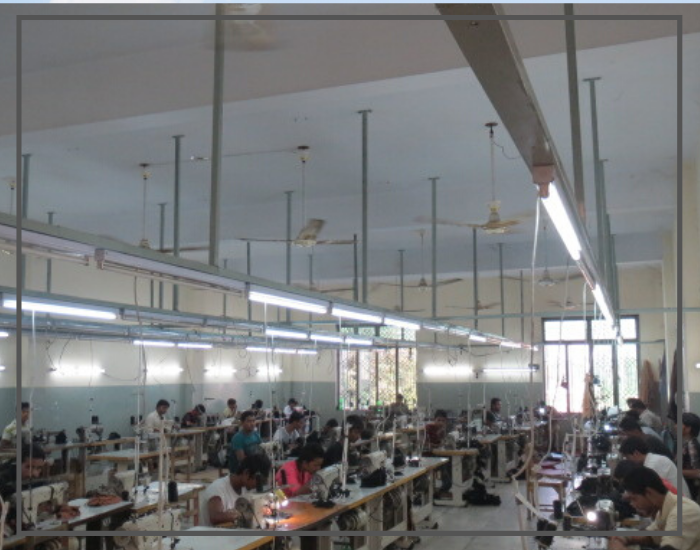
Chain System Stitching Line for Gym Tank Tops
02

Specialized Production Machinery

Equipped with specialized 4-needle 6-thread flatlock machinery, high-speed automated spreading tables, hydraulic die-cutting presses, and heavy-duty boiler steam presses specifically tuned for stretch knits.

In-House Fabric Quality Control Laboratory
03

Lab-Verified Material Quality

Every roll of fabric is quarantined upon arrival. We test for GSM tolerance (±3%), dimensional stability post-wash, colorfastness under perspiration (ISO 105-E04), and anti-pilling resistance prior to marker cutting.

Merchandising & Technical Support Team
04

Dedicated English Merchandising

One dedicated technical merchandiser coordinates your account from initial tech pack review to final bill of lading. Receive weekly photographic milestone updates at cutting, stitching, and pre-shipment stages.

Our Documented 6-Stage Quality Assurance Workflow

Every purchase order follows a strict milestone checklist before moving to the next line station.

Fabric Inspection and GSM Testing

Stage 01: Raw Material Inspection & GSM Clearance

Incoming knit fabrics are audited on inspection tables with backlighting to detect yarn slubs, dye streaks, or elastane breaks. Substandard rolls are rejected immediately.

  • Lot-wise GSM check and width verification
  • Color matching against Pantone / buyer swatches under D65 light box
  • Perspiration and wash colorfastness testing
Hydraulic Press Cutting and Bundle Numbering

Stage 02: CAD Marker Planning & Bundle Numbering

Optimized computer-aided marker layouts ensure minimal fabric waste. Cut panels are shade-numbered in sequential bundles to eliminate shade variation within finished garments.

  • Marker efficiency verified before fabric spreading
  • Shade-grouping to prevent color mismatches across panels
  • Hydraulic precision die-cutting for armhole and neck curves
4-Needle 6-Thread Flatlock Stitching Machine

Stage 03: Chain-System Assembly & In-Line Roving QC

Garments flow through specialized stitching modules. Quality auditors inspect stitches-per-inch (SPI), seam elasticity, and neck tape alignment every hour.

  • Flatlock, overlock, and twin-needle coverstitch operations
  • Calibrated needle-breakage tracking and metal detection policy
  • Seam tension testing under max-stretch parameters
Garment Steam Pressing and Trimming

Stage 04: Industrial Steam Pressing & Trimming

High-pressure boiler steam pressing sets the final garment geometry. Loose threads are hand-trimmed and burn-checked, followed by initial measurement checks.

  • Boiler steam pressing on custom aluminum buck forms
  • 100% loose thread inspection and cleaning
  • Dimensional tolerance audit against graded tech pack specs
Packing and AQL 2.5 Pre-Shipment Inspection

Stage 05: Polybagging, Tagging & AQL 2.5 Audit

Garments receive hangtags, barcode stickers, and custom polybagging. QA inspectors execute final random sampling according to ISO 2859-1 (AQL 2.5 Major / 4.0 Minor).

  • Barcode scannability and SKU ratio verification
  • Carton drop-test and moisture-desiccant insertion
  • Third-party inspection agency access (SGS, Intertek, V-Trust)
Pattern Grading and Prototyping R&D

Stage 06: Rapid R&D, Pattern Grading & Tech Pack Creation

Our CAD master technicians translate mood boards or physical samples into graded pattern files within 48 hours, enabling rapid counter-sample delivery in 7 to 12 working days.

  • Digitized pattern scaling across XS through 5XL
  • Custom trim development (silicone pullers, woven labels, tapes)
  • Sublimation color strike-off approvals prior to bulk cut
OEM & ODM Private Label Direct Factory Sourcing

Ready to Scale Your Gym Tank Tops Collection with Proven Manufacturing?

Partner directly with Haraka Sports in Sialkot, Pakistan. Receive rapid tech pack evaluations, certified lab swatches, and competitive factory-direct pricing for your next season.

Inquire Now

// Technical Buyer Knowledge Base //

Frequently Asked Questions by Global Activewear Buyers

Clear, authoritative technical answers addressing common procurement, material selection, quality control, and shipping inquiries.

High-performance gym tank tops intended for intense workouts typically utilize synthetic blends such as 88% Nylon / 12% Spandex or 90% Micro-Polyester / 10% Elastane. These technical synthetic blends offer superior capillary action for moisture wicking, 4-way elastic recovery, and high tensile strength under heavy stretch. For lifestyle athleisure or oversized muscle tanks, 95% combed long-staple cotton blended with 5% elastane (or bamboo-modal blends) provides a soft hand-feel, structural drape, and skin breathability while retaining shape after commercial washing.
Our standard bulk manufacturing MOQ for custom cut-and-sew or custom-dyed gym tank tops ranges between 150 to 300 pieces per style. This quantity can be split across standard sizing ratios (e.g., S, M, L, XL, XXL) and distributed over up to 3 or 4 custom colorways (Pantone matched). For fully sublimated pinhole mesh training tank tops, development runs can start from as low as 50 pieces per style.
Shrinkage and torque are mitigated during textile preparation. All knit fabrics undergo mechanical compacting, pre-shrinking, and stenter heat-setting before entering our cutting room. We perform laboratory wash testing (3 cycles at 40°C) to ensure dimensional shrinkage remains under 3%. Additionally, our CAD pattern technicians align markers strictly with the vertical grain line of the fabric to eliminate spirality and seam twisting during wear.
Yes. Our pattern room is equipped with advanced CAD digitizing and grading software. You can submit physical reference garments, AI-generated concept renders, or complete PDF tech packs. Our pattern masters engineer custom templates for deep-cut drop armholes, curved scalloped bottom hems, Y-back stringer straps, or anatomical compression muscle cuts, ensuring accurate size grading from XS to 5XL.
We provide a comprehensive selection of embellishment options engineered specifically for high-stretch activewear:
  • 3D High-Density Silicone Heat Transfers: Premium tactile finish with up to 400% stretch recovery.
  • Reflective TPU & Metallic Foils: High-visibility trims for low-light indoor/outdoor training.
  • Italian Ink Dye Sublimation: Vibrant, full-coverage graphics integrated into poly-mesh fabrics without impeding breathability.
  • Soft-Hand Screen Prints: Water-based, discharge, and stretch plastisol inks resistant to wash cracking.
  • Woven & Rubber Patching: Custom branded side tabs, hem labels, and silicone grip waistbands.
Fit samples, fabric swatches, and sublimation strike-offs are typically produced and dispatched within 7 to 12 working days following tech pack clearance. Once pre-production samples (PPS) receive your written approval, bulk production requires 25 to 40 calendar days depending on order volume and embellishment complexity. Shipments can be delivered via express air courier (DHL/FedEx, 4-7 days), air freight (7-10 days), or ocean freight (20-35 days) with full export documentation support.
Haraka Sports operates under audited international compliance guidelines that guarantee fair labor practices, safe working conditions, fair wages, and a zero-tolerance policy for child or forced labor. Our quality management system follows ISO standards and executes AQL 2.5 final inspections. We welcome third-party inspection firms (such as SGS, Intertek, or QIMA) to audit sealed cartons at our factory prior to container loading.