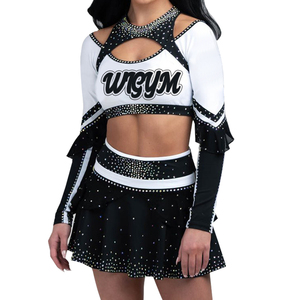
Custom All Star Cheerleading Uniforms Wholesale Bulk Rhinestone Performance Apparel for Team Wear Manufacturer
Inquire Now
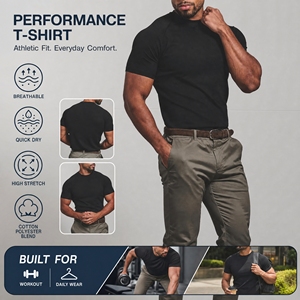
High Quality Performance Muscle Fit t Shirt for Men Raglan Sleeve Activewear Sports Style Fitness Workout Gym Men's T-shirts
Inquire Now
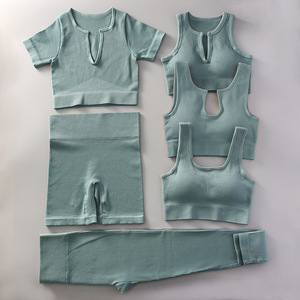
Women 2 Piece Workout Set Stitched Sports Yoga Bra Seamless High Waist Shorts Ladies Gym Fitness Matching Active Tracksuit
Inquire Now
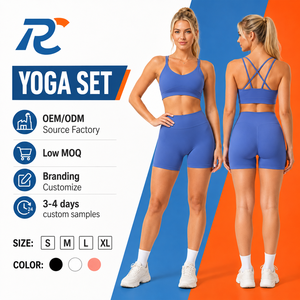
Wholesale Women's High Performance 2pcs Yoga Set Fashionable Seamless Workout Bra Leggings Custom Logo Ladies Fitness Apparel
Inquire Now
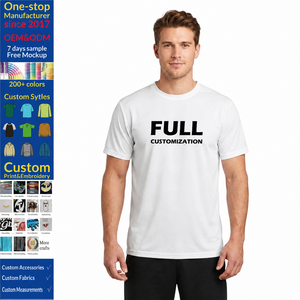
Men's Custom 100% Polyester Performance T-Shirt Quick Dry Loose Fit Knitted Sports Wear Wholesale Running Apparel White Color
Inquire Now
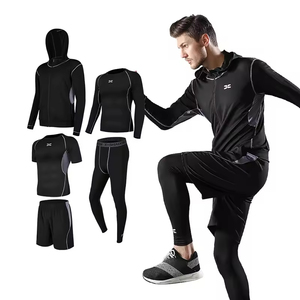
Men's Quick Dry Gym Sports Suit Long Sleeve Fitness Running Clothes with Yoga Tights Three Piece Suit for Spring Season
Inquire Now
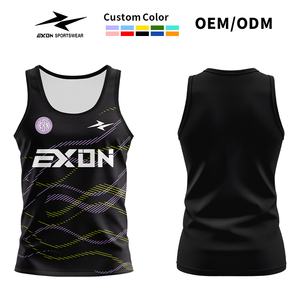
EXON Lightweight Performance Running Singlet with Performance Fabric,professional Vest for Racing Events and Marathon Training
Inquire Now
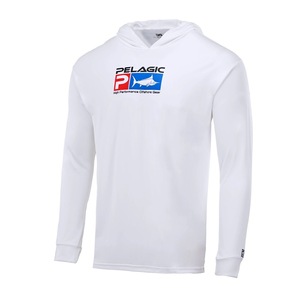
Custom Performance Uv protection Quick Dry Uv Sublimation Wholesale Long Sleeve for Men Hood Fishing t Shirt Jersey
Inquire Now
3rd Gen
Manufacturing Expertise
AQL 2.5
Strict Quality Audits
30+
Global Export Markets
7-12 Days
Rapid Sample Turnaround
Executive Summary: Navigating China's Athletic Socks & Activewear Export Ecosystem
The global market for athletic socks and technical activewear has undergone a structural paradigm shift. No longer viewed as secondary accessories, performance socks—engineered with graduated compression zones, blister-mitigating terry loops, and fiber-level moisture management—have emerged as high-margin hero products for international sportswear brands. As a leading manufacturer and exporter in the region, China remains the global epicenter of technical hosiery innovation, supplying over 65% of high-density circular knitted athletic gear worldwide.
For procurement directors, OEM brand managers, and retail chain buyers, selecting a reliable partner among China top athletic socks suppliers & exporters requires evaluating parameters far beyond FOB price points. Modern sourcing demands complete supply chain transparency, technical needle precision (ranging from 144N to 200N construction), fiber-level verification (such as CoolMax®, Thermolite®, recycled polyamide, and combed cotton), and rigorous AQL 2.5 quality control compliance. This comprehensive whitepaper provides authoritative benchmark data, manufacturing insights, and strategic sourcing frameworks for international buyers.
1. Technical Blueprint: Engineering High-Performance Athletic Socks
True technical athletic socks are marvels of biomechanical textile engineering. Unlike lifestyle hosiery knitted on standard 108-needle or 120-needle machines, high-performance athletic socks utilize advanced 144N, 168N, and 200N computer-controlled single and double-cylinder knitting machinery. The higher needle density allows for intricate target padding, anatomical left/right foot shaping, dynamic arch support bands, and seamless hand-linked toe closures.
Our integrated manufacturing facilities employ state-of-the-art Italian and Lonati-style automated knitting units capable of multi-zone elastomeric inlaying. This ensures engineered graduated compression profiles that stabilize the plantar fascia, reduce muscle vibration during endurance activities, and accelerate post-workout recovery.
| Performance Class |
Needle Count (N) |
Primary Material Blend |
Key Structural Features |
Ideal Application |
| Pro Marathon & Running |
200N Fine Gauge |
55% CoolMax / 35% Nylon / 10% Spandex |
Hand-linked seamless toe, anti-blister mesh zones, heel tab padding |
Distance Running, Trail Racing |
| Basketball & High-Impact |
168N Heavy Terry |
70% Combed Cotton / 22% Polyester / 8% Elastane |
High-density sole cushion, ankle bone protection, arch compression band |
Basketball, Court Sports, Training |
| Cycling & Aerodynamic |
200N / 240N Ultra-Fine |
80% Polyamide / 20% Elastane (Lycra®) |
Aerodynamic ribbed cuff, ultra-breathable instep, zero-slip compression band |
Road Cycling, Triathlon |
| Outdoor Trekking & Winter |
144N Double Cylinder |
45% Merino Wool / 35% Acrylic / 15% Nylon / 5% Elastane |
Full-foot loop terry heat retention, rib-knit leg warmth, reinforced toe/heel |
Mountaineering, Cold-Weather Workwear |
Integrated Manufacturing Excellence: From Yarn to Shipped Container
Building upon decades of textile manufacturing heritage—originally refined across our multi-generational production facilities—our operations incorporate a fully integrated OEM/ODM workflow. Sourcing directly from certified yarn spinners allows us to maintain strict lot-to-lot consistency, preventing micro-shading and elasticity drift across large-scale production orders.
R&D & Material Innovation
Continuous testing of antimicrobial copper-infused yarns, recycled GRS-certified polyesters, and bio-based moisture-wicking polymers to give private labels a competitive information gain.
Six-Stage Quality Assurance
Every lot undergoes yarn GSM verification, needle audit, in-line roving checks, steam board sizing, metal detection, and final end-line AQL 2.5 random carton audits.
Agile ODM Development
Rapid 7-12 day sample prototyping for custom logos, jacquard patterns, sublimation prints, and silicone anti-slip leg grippers before mass production authorization.
2. Quality Control & Compliance Framework
For international buyers importing into North America, Europe, and Australasia, regulatory compliance is non-negotiable. Non-compliant dyes or hazardous chemical residues can lead to costly border detentions and brand reputational damage. Our manufacturing protocols comply strictly with OEKO-TEX® Standard 100, REACH, and BSCI social compliance standards.
Each incoming yarn shipment is subjected to dimensional stability testing (shrinkage control within ±3% after 20 commercial wash cycles), color fastness to rubbing and perspiration (Grade 4-5 minimum), and pilling resistance evaluation using Martindale abrasion testers. This meticulous approach guarantees that products sold under your brand deliver flawless performance, reduced return rates, and high end-user satisfaction.
Future Procurement & Supply Chain Trends (2025–2030)
Understanding future industry vectors enables procurement managers to build resilient, forward-looking product lines. As search intent and consumer demand evolve toward functional performance and environmental stewardship, three core trends dominate the global athletic socks sourcing horizon:
Trend 1: Eco-Responsible & Circular Materials
The transition from virgin synthetic fibers to post-consumer recycled polymers is accelerating. Leading global brands now mandate minimum thresholds of 50% GRS-certified (Global Recycled Standard) recycled nylon and Repreve® polyester. In response, our knitting lines have been re-calibrated to process high-tenacity recycled filament yarns without sacrificing tensile strength or elasticity.
Trend 2: Seamless Zone-Mapping & Hybrid Fabrics
Modern consumers demand lightweight, multi-functional socks that transition seamlessly between gym workouts, office environments, and outdoor endurance activities. Hybrid fiber blending—combining natural temperature-regulating Merino wool with durable elastane-core nylon—allows for year-round temperature control, odor resistance, and long-term shape retention.
Trend 3: Smart Textiles & Anti-Slip Silicone Injection
The rapid rise of specialized grip socks across soccer, pilates, and yoga markets has driven demand for high-friction silicone application. Using computerized liquid silicone injection machines, we apply durable 3D grip arrays directly to the sock sole, ensuring enhanced traction, rapid directional stability, and zero slippage inside athletic footwear.
Why Partner With Us: Corporate OEM & ODM Competitive Edge
Navigating global procurement requires a partner who combines modern manufacturing capabilities with clear communication and strict deadline adherence. Here is why international buyers choose our facilities as their preferred supplier in China:
-
Flexible Low MOQs for New Brand Lines: We support growth-stage brands by offering lower minimum order quantities (starting from 150–300 units for cut-and-sew and 500 pairs per colorway for customized knitted socks).
-
Full Packaging & Private Label Integration: From custom paper bands, header cards, and recycled polybags to barcode labeling and ready-to-shelf retail display cartons, we deliver a turnkey solution.
-
Transparent Merchandising & Live Reporting: Dedicated English-speaking account managers provide weekly production updates, step-by-step milestone photos, and clear shipping timelines.
-
Consolidated Global Freight Solutions: Strategic proximity to major international ports (Ningbo/Shanghai/Shenzhen) allows us to offer flexible DDP, FOB, CIF, or express air transport options.
Frequently Asked Questions (FAQ) for Global Procurement Buyers
Below are authoritative answers to common inquiries raised by international buyers, brand owners, and supply chain directors regarding custom athletic socks production and export logistics.
What is the standard lead time for sampling and bulk mass production?
Fit samples, yarn strike-offs, and jacquard artwork proofs are typically delivered within 7 to 12 working days following tech pack confirmation. Bulk mass production requires 25 to 40 calendar days depending on custom yarn dyeing requirements, needle complexity, order volume, and packaging customization.
What needle count (N) should we choose for our athletic sock line?
Needle count depends on the intended end-use. 144N is ideal for thick cushion socks, outdoor hiking, and casual crew styles. 168N represents the ideal industry standard for basketball, football, and everyday workout socks. 200N fine-gauge construction is recommended for ultra-light marathon running, cycling, and premium dress socks requiring high-definition logo jacquards.
Do you support private label custom branding and custom packaging?
Yes, complete private label development is our core specialty. We offer custom jacquard logo knitting, high-density silicone heat transfer logos, woven labels, embroidered cuffs, printed rider cards, eco-friendly hangtags, and branded retail display boxes built precisely to your artwork tech pack.
How do you ensure consistent sizing and elastic recovery across production runs?
We utilize precise digital steam-boarding forms matched to international sizing standards (US, EU, UK, JP). Additionally, we use high-grade Lycra® spandex cores in our elastic bands, which undergo rigorous fatigue-stretch testing to maintain shape recovery even after 30+ industrial wash cycles.
Can we request third-party quality inspections prior to container loading?
Absolute transparency is guaranteed. We welcome third-party inspection agencies such as SGS, BUREAU VERITAS, Intertek, or your nominated local audit agent to inspect production lots at any stage—including raw material receiving, in-line stitching, or final sealed container loading.
Ready to Elevate Your Athletic Socks & Activewear Sourcing?
Connect directly with our senior engineering and merchandising team to request physical sample swatches, factory audit documentation, or an immediate quotation for your upcoming season.
Inquire Now