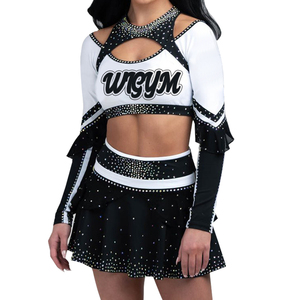
Custom All Star Performance Team Wear & Apparel
Heavy-duty technical knit and embellished team wear with moisture-wicking properties and reinforced flatlock stitching.
Send an Inquiry
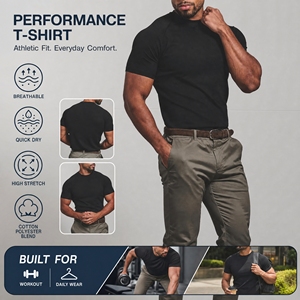
High Quality Performance Muscle Fit Activewear Shirt
Raglan sleeve athletic gym wear engineered with 4-way stretch poly-spandex blend for intense workout recovery.
Send an Inquiry
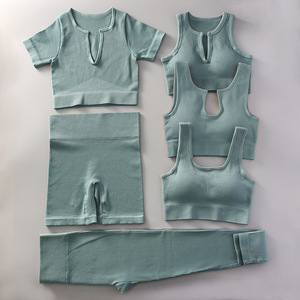
Women's 2-Piece Seamless High-Waist Athletic Set
Precision circular-knit activewear set providing targeted compression zones and breathable thermal regulation.
Send an Inquiry
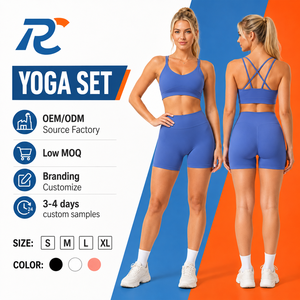
Custom Logo High-Performance Seamless Yoga & Gym Set
Private label squat-proof fitness wear featuring high-elastane density and customized heat-transfer branding.
Send an Inquiry
Men's Quick-Dry Micro-Mesh Athletic Running Shirt
Lightweight loose-fit knitted training wear with anti-pilling and rapid evaporative moisture channels.
Send an Inquiry
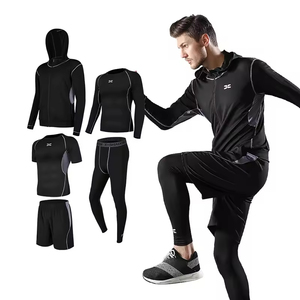
Men's Multi-Piece Gym Training & Compression Suit
Complete athletic kit comprising compression tights, outerwear jacket, and breathable technical base layers.
Send an Inquiry
Pro Racing Marathon Singlet & Ultra-Light Top
Ultralight aerodynamic racing vest constructed with friction-reducing edge bonding for marathon events.
Send an Inquiry
Custom UV Protection Sublimated Outdoor Jersey
UPF 50+ long-sleeve athletic jersey with vibrant full-dye sublimation and integrated sun-protection hood.
Send an Inquiry
25M+
Annual Pair Capacity
AQL 1.5
Quality Assurance Standard
50+
Global Export Markets
Technical Whitepaper: Sourcing High-Performance Sports Socks & Athletic Apparel from China Manufacturers
In the modern global athletic footwear and apparel industry, technical sports socks have evolved from basic commoditized hosiery into biomechanically engineered performance equipment. B2B buyers, sourcing managers, and private label apparel brands operating in tier-1 markets require deep supply chain visibility, precision yarn formulation, advanced cylinder needle specifications, and rigorous quality compliance to remain competitive.
As a leading China Wholesale Sports Socks Manufacturer & Exporter, our facility integrates decades of manufacturing heritage with state-of-the-art circular knitting technology. This comprehensive sourcing guide outlines the technical paradigms, fiber selection matrices, quality assurance protocols, and market projections necessary for high-volume B2B buyers to optimize their product lines while maximizing gross margins.
1. Fiber Architecture & Functional Material Sourcing
The foundation of any high-performance sock lies in its raw yarn composition. Advanced moisture management, thermal regulation, friction reduction, and durability cannot be achieved through generic cotton yarns. We utilize a targeted multi-fiber matrix engineered for specific athletic disciplines:
Utilizing specialized micro-groove polyesters (CoolMax®, Dryarn®) and high-tenacity Nylon 6,6 to push sweat away from skin surface via capillary action, preventing skin maceration during high-end endurance sports.
Integration of Silver-Ion (Ag+) embedded threads and bamboo-derived viscose fibers. Inhibits 99.9% of odor-causing bacteria (Staphylococcus aureus) across 50+ industrial wash cycles.
Covered DuPont Lycra® spandex strategically mapped at 140D to 210D tension levels. Ensures dynamic arch compression, ankle stabilization, and zero slip during sudden lateral cuts.
2. Machinery Needle Counts & Gauge Specifications
Selecting the correct cylinder needle count defines sock density, cushioning thickness, and graphic resolution. Our manufacturing setup features computer-controlled Lonati and Santoni Italian circular knitting machines ranging from 96N to 200N gauge configurations:
| Needle Count (Gauge) |
Primary Athletic Category |
Fabric Density & Thickness |
Key Performance Benefit |
| 96N - 108N |
Heavy Workwear & Extreme Outdoor Boots |
Ultra-Thick Terry Loop (>450 GSM) |
Maximum impact absorption & thermal insulation |
| 144N - 156N |
Basketball, Soccer & Cushion Tennis Socks |
Medium-Heavy Density (320 - 400 GSM) |
Plush footbed protection & durable friction barriers |
| 168N |
Multi-Sport Training & Cycling Apparel |
Balanced Fine Density (260 - 320 GSM) |
Smooth jacquard detailing & mid-foot compression |
| 200N High-Gauge |
Pro Marathon Running & Medical Compression |
Ultra-Fine Micro-Knit (<240 GSM) |
Featherweight fit, zero blister risk, crisp high-def logos |
3. Anatomical Podiatry Engineering & Zone-Mapping
Modern consumers demand ergonomic comfort. Our OEM development team utilizes 3D CAD zone-mapping to build socks that conform perfectly to left and right foot morphology (L/R Ergonomics):
- Metatarsal & Heel Impact Zones: High-density density terry loops padded specifically over the calcaneus and ball of the foot to absorb shock loads exceeding 3x bodyweight.
- Self-Adjusting Arch Support Band: Ribbed elastic webbing surrounding the midfoot, actively preventing plantar fascia fatigue and restricting sock rotation inside athletic shoes.
- Seamless Hand-Linked Toe (Linking Tech): Eliminates the bulky traditional hand seam across the toe box. By employing automated computer linking (Rosso / Hand-Linking machines), we achieve 100% flat seams that eliminate friction blisters.
- Aero-Mesh Ventilation Windows: Open-weave honeycomb structures engineered onto the top instep, allowing rapid heat dissipation and dry air influx during peak exertion.
Operating over 35,000 sq.m of manufacturing floor space equipped with 400+ automated knitting machines, wet-finishing plants, and automated boarding systems.
Rigorous 6-tier quality protocol from raw yarn batch testing (GSM, color fastness, pilling) to in-line roving checks and final pre-shipment box audits.
Complete private-label execution: custom jacquard knitting, silicone grip application, woven labels, heat-transfer logos, and eco-friendly packaging boxes.
Certified factory operations meeting OEKO-TEX® Standard 100, BSCI, and ISO 9001 standards with export expertise to over 50 countries worldwide.
6-Stage Precision Quality Control Workflow
Every purchase order follows a strict, fully documented quality chain. Nothing proceeds to subsequent manufacturing stages without QA sign-off:
Stage 01
Raw Yarn Verification
Yarns quarantined & audited for denier uniformity, tensile strength, color fastness to wash/rubbing, and chemical safety compliance.
Stage 02
Cylinder Tension Calibration
Knitting machines calibrated for exact stitch density, loop height, and elastane feeding speed per approved tech packs.
Stage 03
Seamless Toe Linking
100% inspection of toe-closure seams (Rosso or Hand-Linked) to ensure zero protrusion and smooth internal finish.
Stage 04
Thermal Boarding & Pre-Shrinkage
High-pressure steam boarding sets final shape dimensions, stabilizes fabric elasticity, and prevents post-wash shrinkage.
Stage 05
In-Line & Metal Detection Inspection
Every single pair passes needle-detector sensors to guarantee zero metallic fragment contamination prior to pairing.
Stage 06
Final AQL 1.5 Box Inspection
Random unannounced sampling of sealed master cartons verifying assortment ratio, barcodes, hangtags, and packaging integrity.
Future Global Sourcing & Manufacturing Trends (2025–2030 Whitepaper Forecast)
To assist apparel brand directors, sourcing agents, and wholesale buyers in long-term strategic planning, our research team has compiled key industry vector shifts shaping sports sock manufacturing over the coming decade:
Trend 1: Circular Eco-Synthetics & Traceable Recycled Fibers
Environmental legislation in the EU (Digital Product Passport) and North America is making sustainable material sourcing mandatory. Brand buyers are moving away from virgin synthetics toward Global Recycled Standard (GRS) certified Recycled Nylon 6,6 and rPET (recycled polyester from ocean-bound plastics). In response, our facility has established certified closed-loop supply chains offering 100% GRS-compliant yarns paired with biodegradable elastane technology that breaks down in landfills within 3 years without releasing microplastics.
Trend 2: Micro-Zoned Graduated Medical Compression
The convergence of athletic performance wear and medical compression is accelerating. Future athletic socks are incorporating graduated compression profiles (15-20 mmHg to 20-30 mmHg) engineered to enhance venous return, accelerate lactate clearance, and mitigate deep vein thrombosis (DVT) during long team travel. Manufacturing these garments requires electronic tension-controlled feeding units that adjust spandex tension stitch-by-stitch down the leg column.
Trend 3: Smart Textiles & Phase-Change Thermoregulation
Next-generation socks are incorporating micro-encapsulated Phase Change Materials (PCMs) within the synthetic matrix. These paraffin-based micro-capsules absorb thermal energy when skin temperature rises and release heat when the body cools down, maintaining an ideal cutaneous temperature of 32°C. Advanced sensor-ready pockets for foot-strike podiatry tracking are also entering high-performance running segments.
Trend 4: Supply Chain Agility & Flexible Minimum Order Quantities (MOQs)
The traditional model of ordering 10,000 pairs per colorway is being replaced by agile, low-inventory procurement models. Utilizing modular digital knitting setups, our factory empowers buyers to initiate test-market runs from 500 to 1,000 pairs per style with rapid replenishment cycles within 15–20 days, drastically reducing inventory holding costs and overstock markdown risks.
Strategic Comparison: Legacy Socks vs. Next-Gen Technical Sports Socks
| Feature Parameter |
Legacy Wholesale Sports Socks |
Next-Gen Technical Sports Socks (Our OEM Standard) |
| Fiber Formulation |
100% Carded Cotton or Basic Virgin Poly |
Technical Blends (CoolMax, Merino Wool, Silver Ag+, GRS Nylon) |
| Toe Construction |
Bulky Machine Stitched Seam (Rosso) |
100% Flat Hand-Linked Seamless Toe Box |
| Fit Mechanics |
Symmetrical Tubing (Tube Socks) |
Anatomical Left/Right (L/R) Ergonomic 3D Contour Mapping |
| Elastane Retention |
Standard Rubber Elastic (Degrades rapidly) |
High-Durability Covered DuPont Lycra® (100+ Wash Retention) |
| Arch & Ankle Support |
Uniform Compression Throughout |
Micro-Zoned Targeted Arch Compression & Ankle Locking Ribs |
What is your Minimum Order Quantity (MOQ) for custom private label sports socks?
Our standard minimum order quantity for custom jacquard or sublimated sports socks starts at 500 to 1,000 pairs per style/colorway, split across standard size runs (e.g., S, M, L, XL). For specialized yarn formulations (such as custom-dyed pantone colors or merino wool blends), MOQs range from 2,000 to 3,000 pairs depending on raw material mill minimums.
What is the lead time for sampling and mass bulk production?
Physical sample prototypes and yarn strike-offs are typically completed within 7 to 10 working days following digital tech pack sign-off. Bulk mass production lead times range from 25 to 35 days depending on order volume, packaging complexity, and raw material availability. Repeat re-orders on existing patterns run on an accelerated 15-to-20-day production timeline.
Do you offer full custom packaging and branding development?
Yes. We provide complete end-to-end ODM private label packaging solutions. Options include custom printed paper header cards, wrap-around bands, embossed cardboard gift boxes, polybags with custom warning print/barcodes, metallic hook attachments, and eco-friendly biodegradable packaging. Our design team can work directly from your vector artworks.
What yarn certifications and factory compliance standards do you possess?
Our manufacturing facilities operate under strict global social and environmental compliance protocols. We maintain current audits for BSCI, SMETA (SEDEX), ISO 9001:2015, and our raw materials carry OEKO-TEX® Standard 100 and Global Recycled Standard (GRS) certifications, guaranteeing zero hazardous chemicals or banned azo dyes in finished goods.
How do you handle color matching and pantone accuracy?
We utilize the international Pantone Matching System (PMS Textile Cotton TPX/TCX). Dyed yarn lots undergo spectrophotometer color testing under multiple light sources (D65, TL84, CWF) to ensure a minimum Delta E (ΔE) variance of < 1.0 against buyer-approved swatches before knitting commences.
Can you consolidate sports socks shipments with other activewear garments?
Absolutely. Because our industrial group operates integrated apparel and knitwear divisions, buyers can consolidate shipments combining performance socks, seamless yoga sets, gym tops, hoodies, and team uniforms into single FCL/LCL container shipments, drastically cutting freight costs and simplifying import customs clearance.
Partner with China's Premier Sports Socks Manufacturer
Ready to upgrade your sock lines with technical fiber science, zero-defect quality control, and competitive direct-factory pricing? Connect with our senior merchandising team today for tech pack reviews, sample requests, and instant quote estimates.
Send an Inquiry