B2B Sourcing Guide, Technical Textiles & Global Supply Chain Report
Featured Manufacturing Catalog
High-Performance Activewear & Gymwear Range
Engineered for global private label brands, athletic teamware distributors, and commercial gym chains. Fully customizable with low MOQs and certified AQL 2.5 quality control.
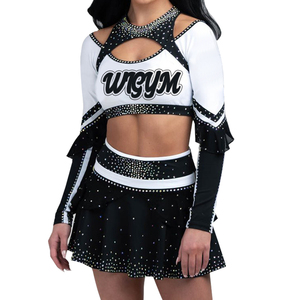
Custom All Star Cheerleading Uniforms Bulk Rhinestone Performance Apparel
The Strategic Evolution of OEM Gymwear Sourcing: A B2B Manufacturing Whitepaper
The global activewear and gymwear market is undergoing a paradigm shift driven by technological advancement in synthetic fibers, heightening consumer expectations for sustainability, and extreme demands for supply chain agility. For procurement directors, brand owners, and apparel wholesalers, selecting a custom OEM gymwear factory is no longer merely a pricing exercise—it is a strategic decision that dictates product performance, brand equity, and speed-to-market resilience.
"Modern activewear buyers require more than basic cut-and-sew capacity. Success in today's market demands direct factory integration, 3D pattern prototyping, verifiable fiber traceability, and rigid AQL quality controls built directly into the assembly line."
1. Advanced Technical Textiles & Material Engineering Trends
Performance gymwear has evolved far beyond standard cotton-polyester blends. Technical activewear now functions as an athletic performance tool, leveraging bio-mechanical engineering, thermal management, and elastomeric integrity. Premier OEM gymwear exporters must master diverse textile parameters to satisfy high-performance specifications:
Spandex/Elastane core-spun nylon yarns preventing sagging at knee and elbow flex zones.
Moisture Vapor Transmission (MVTR)
> 10,000 g/m²/24h
Micro-channel hydrophobic poly fibers directing moisture away from dermis to garment surface.
Seam Tensile Strength
ISO 13935-2 Flatlock Stitching
6-needle 4-thread flatlock construction ensuring zero chafing and high burst resistance under load.
Color Fastness Rating
Grade 4-5 (ISO 105-C06)
High-temperature disperse sublimation inks resistant to heavy friction and acidic sweat erosion.
2. Seamless Knitting vs. Cut-and-Sew Assembly Dynamics
One of the primary decisions in gymwear product development is choosing between 3D circular seamless knitting and specialized cut-and-sew construction. Custom OEM factories must maintain parallel production infrastructure to support both modalities:
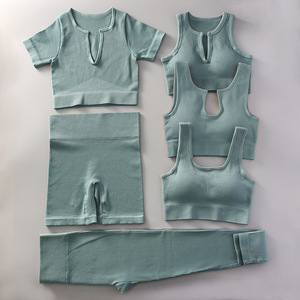
3D Circular Seamless Technology: Utilizing Santoni-style circular knitting machines, seamless apparel integrates targeted compression zones, ventilation mesh, and elastic support directly into a single continuous tube of fabric. This eliminates 80% of assembly seams, minimizing friction points for high-intensity training (HIIT), yoga, and running. It also reduces fabric cutting waste to virtually zero.
Engineered Cut-and-Sew Flatlock Construction: For structured garments, team uniforms, outer jackets, and heavy lifting apparel, cut-and-sew remains irreplaceable. By combining pre-dyed or sublimated panel cuts with ergonomic paneling, flatlock stitching provides targeted structural support, custom color blocking, and precise pattern grading for extreme size inclusivity.
The legacy sourcing model of ordering 10,000 pieces per style with 6-month lead times is rapidly becoming obsolete. Contemporary activewear brands operate under lean inventory models (VMI and QR) to mitigate overproduction risk. Forward-thinking OEM gymwear exporters in Sialkot and global hubs are implementing structural shifts to support this new paradigm:
Agile Minimum Order Quantities (MOQs): Offering flexible production tiers from 50 pieces per style for custom sublimated teamwear to 150-300 pieces for complex cut-and-sew activewear lines.
Digital CAD & 3D Virtual Prototyping: Utilizing digital pattern software to render photorealistic 3D samples, cutting physical sample iteration cycles from weeks to under 48 hours and drastically cutting fabric waste.
Sustainable Polymer Infrastructure: Transitioning from virgin synthetics to Global Recycled Standard (GRS) certified Recycled Polyester (rPET) derived from post-consumer water bottles, alongside eco-friendly OEKO-TEX Standard 100 non-toxic dye formulations.
Our Production Advantage
Vertically Integrated Manufacturing Facilities
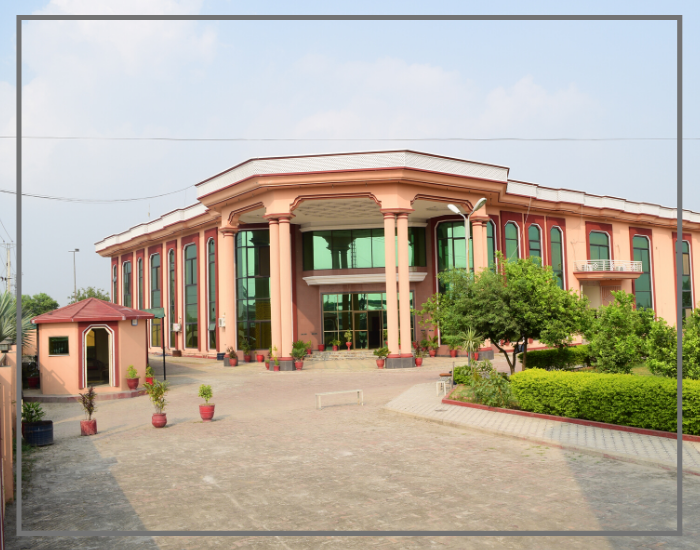
Operating out of Sialkot, Pakistan's world-renowned athletic apparel export hub, Haraka Sports combines three generations of family craftsmanship with modern industrial automation.
PILLAR 01
Company Profile & Heritage
A third-generation family-owned exporter built on long-term client partnerships. Operating two main production complexes (Daska Road Head Office and Small Industries Estate Unit) serving buyers across 30+ countries.
PILLAR 02
Production Capacity & Lines
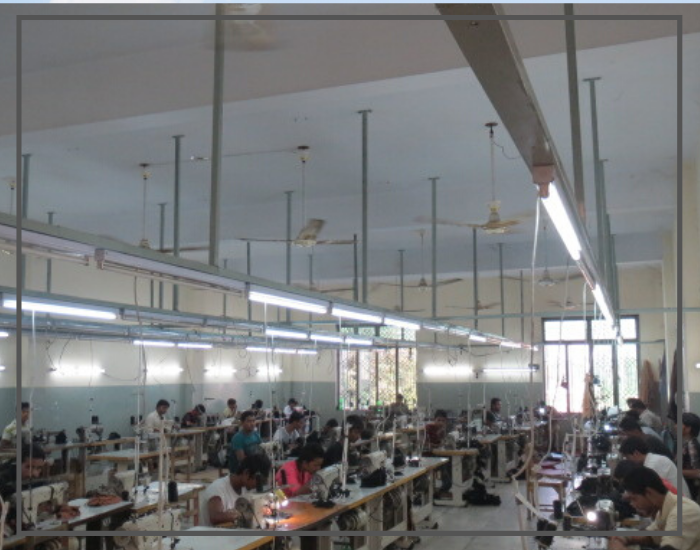
Equipped with specialized chain-system stitching lines, hydraulic press cutters, continuous sublimation heat presses, and automated leather/nylon stitchers for parallel multi-category production runs.
PILLAR 03
Rigid Quality Assurance
Systematic raw material quarantine, in-line roving inspections, and final AQL 2.5 pre-shipment audits. Defect logging ensures complete traceability and zero repeated assembly faults.
PILLAR 04
Dedicated Account Merchandising
Every account is paired with an English-speaking technical merchandiser who delivers weekly photo-documented milestone reports from cutting through to final carton loading.
6-Step Quality Control Protocol
Documented Production Workflow
From raw fabric roll to container seal, every purchase order passes through six audited production checkpoints.
01
1. Fabric Inspection & Testing
Incoming knit and woven lots undergo lab testing for GSM weight, elasticity recovery, shrinkage allowance, and color fastness before store release.
02
2. Precision CAD Cutting
Automated marker planning maximizes fabric yield. Panels are cut via hydraulic press or vertical knife and sequentially numbered to prevent shade variation.
03
3. Specialized Chain Stitching
Operated on a specialized unit system where technicians handle distinct flatlock, overlock, or bartack operations with hourly QC roving audits.
04
4. Boiler Steam Finishing
Garments undergo boiler steam pressing for dimensional stabilization, complete thread trimming, logo alignment audits, and measurement checks.
05
5. AQL 2.5 Pre-Shipment Audit
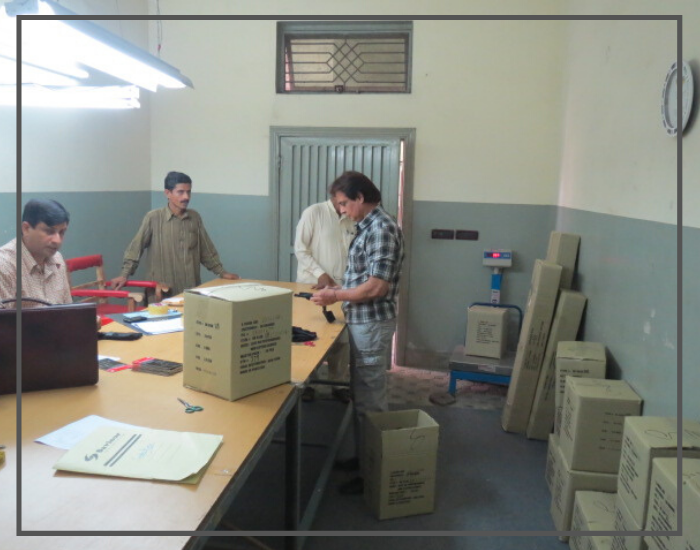
Final random sampling of individual sealed cartons. Barcode scan verification, ratio confirmation, and polybag artwork compliance checks.
06
6. R&D & Pattern Engineering
Continuous material innovation, pattern grading room, custom print strike-offs, and rapid prototype turnarounds within 7-12 business days.
Procurement Knowledge Base
Custom OEM Gymwear Sourcing FAQ
Answers to key commercial and technical questions from international sourcing managers and apparel brand directors.
What are the typical Minimum Order Quantities (MOQs) for custom gymwear orders?
For fully sublimated teamwear (such as basketball kits, soccer jerseys, and cycling apparel), our minimum development runs start at 50 pieces per style. For custom cut-and-sew activewear, seamless leggings, and fleece knitwear programmes, standard production batches start at 150 to 300 pieces per style, which can be split across standard size runs (XS-XXL) and up to four colorways.
What is the lead time for fit sampling, sublimation strike-offs, and bulk production?
Fit samples, physical strike-offs, and fabric swatches are typically dispatched within 7 to 12 working days following tech pack and artwork approval. Mass production lead time ranges between 25 and 40 days, depending on fabric mill development, embellishment complexity (e.g., silicone heat transfers vs. high-density embroidery), and overall order quantity.
Do you provide complete private label and ODM collection development?
Yes. Our in-house design and pattern team works directly with client mood boards, CAD sketches, or physical reference garments to create graded technical specifications. We handle all private label branding, including woven neck labels, reflective heat-seal transfers, custom printed hangtags, barcoded polybags, and custom packing cartons.
What quality standards and factory compliance audits are supported?
Every incoming raw material lot is audited for GSM weight, dimensional shrinkage, color fastness, and anti-pilling resistance. Bulk production follows documented AQL 2.5 final inspection protocols. Furthermore, our facilities adhere to strict social compliance standards, and third-party inspection agencies (such as SGS, Bureau Veritas, or Intertek) are welcome to perform pre-shipment audits.
Can different product categories (e.g., activewear, knitwear, and lifting belts) be consolidated?
Because we operate integrated production facilities across sportswear, activewear, fleece knitwear, outerwear, and leather/nylon fitness gear in Sialkot, clients can consolidate multiple product lines into a single export container or shipment. This significantly lowers sea/air freight overheads and simplifies customs documentation for overseas buyers.
Ready to Scale Your Gymwear Line direct from Factory?
Partner with a proven 3rd-generation OEM/ODM manufacturer. Submit your tech pack or request physical samples today.