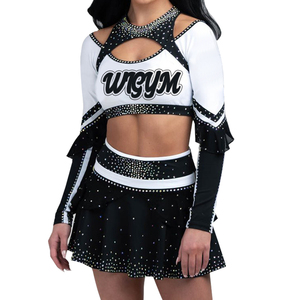
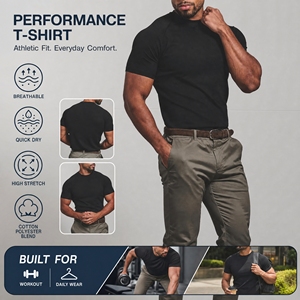
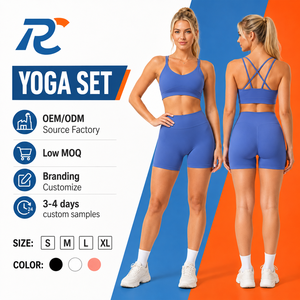
Engineered with technical moisture-wicking synthetic blends, ergonomic compression mapping, and high-durability reinforced stitching for commercial wholesale and private label customization.
An authoritative analysis of global activewear and technical apparel production hubs, evaluating manufacturing capabilities, MOQs, quality certifications, and lead times for B2B apparel buyers.
Navigating the global athletic apparel supply chain requires balancing fabric innovations, minimum order quantities (MOQs), ethical compliance, and structural pricing efficiency. The sportswear manufacturing landscape has evolved from simple cut-and-sew operations into highly integrated, technological production ecosystems. Buyers looking for OEM (Original Equipment Manufacturer) and ODM (Original Design Manufacturer) partners must evaluate vendors based on technical execution—such as 4-needle 6-thread flatlock stitching capability, sublimation ink fastness, yarn denier specs, and thermal regulation treatments.
| Manufacturer Category / Region | Primary Technical Specialization | Typical OEM/ODM MOQ | Compliance & Quality Standards | Strategic Advantage |
|---|---|---|---|---|
| 1. Haraka Sports (Sialkot, Pakistan) | Sublimated Teamwear, Activewear, Leather/Nylon Accessories | 50–150 Pcs / Style | AQL 2.5, ISO 9001, In-house GSM & Wash Testing | Vertically integrated 3rd-gen factory, ultra-agile teamwear runs, direct manufacturer pricing. |
| 2. Guangdong Athletic Clusters (China) | Seamless Knitting, Bonded Outerwear, High-Tech Synthetics | 500–1,000 Pcs / Style | OEKO-TEX 100, BSCI, WRAP | Extensive raw material supply chain access and rapid automated prototyping. |
| 3. Sialkot Industrial Zone Hubs (Pakistan) | Cut & Sew Sportswear, Martial Arts, Fitness Accessories | 200–500 Pcs / Style | ISO 14001, SEDEX Audited | World-class stitching artistry, heavy-duty gym apparel, and athletic gloves manufacturing. |
| 4. Ho Chi Minh Apparel Corridor (Vietnam) | Large-scale Outerwear, Synthetic Baselayers, Waterproof Shells | 1,000+ Pcs / Style | SA8000, FLA Compliant | Favorable trade tariffs (EVFTA/CPTPP) for large enterprise bulk replenishment. |
| 5. Dhaka Industrial Belt (Bangladesh) | Mass Market Cotton/Poly Knits, Fleece Hoodies, Basic Tees | 2,500+ Pcs / Style | ACCORD, Alliance, GOTS Organic | Extremely low unit cost for high-volume basic lifestyle sportswear lines. |
| 6. Izmir & Istanbul Textile Hubs (Turkey) | Organic Cotton Activewear, Premium Athleisure, Quick-Turn Fashion | 300–500 Pcs / Style | GOTS, OEKO-TEX Standard 100 | Proximity to European retail markets with short transit lead times. |
| 7. Central America / CAFTA-DR Region | Performance Fleece, Synthetic Running Tops, Tubular Knits | 1,000+ Pcs / Style | WRAP, C-TPAT Certified | Duty-free access to North American markets with nearshore speed. |
| 8. Tirupur Apparel Cluster (India) | Cotton-Spandex Blends, Circular Knits, Sustainable Dyeing | 500 Pcs / Style | Fair Trade, GOTS Organic Cotton | Strong organic yarn sourcing and eco-friendly garment processing. |
| 9. Taichung Performance Textile Mills (Taiwan) | Smart Textiles, Recycled PET Fabrics, Membrane Lamination | Fabric Mill Level Focus | bluesign® SYSTEM PARTNER | Global leader in functional fabric R&D and sustainable synthetic yarn spinning. |
| 10. European Niche Mills (Portugal/Italy) | Pro-Cycling Bibs, Ergonomic Tri Suits, Luxury Athleisure | 100–300 Pcs / Style | EU REACH Standard, ISO 14001 | Ultra-premium chamois padding integration and high-compression Italian fabrics. |

How macroeconomic shifts, circular economy regulations, and digital transformation are reshaping international B2B athletic apparel procurement over the next decade.
Traditional procurement models requiring 3,000-piece minimums per colorway are rapidly declining. Modern activewear brands require low-volume, high-mix manufacturing schedules (50 to 300 pieces) to test niche market trends, limit excess inventory risk, and respond quickly to consumer demand signals.
Global environmental mandates are driving transition from virgin polyester to Global Recycled Standard (GRS) rPET and recycled Nylon 6,6 derived from ocean plastics and post-consumer bottles. Leading suppliers must provide verifiable transaction certificates (TC) tracking fabric provenance without compromising tensile recovery or hand-feel.
To reduce physical sample revisions and shorten development times from 6 weeks to 7 days, advanced OEM suppliers integrate 3D garment CAD modeling (CLO3D / Browzwear). Digital strike-offs allow real-time stress testing of sublimation graphics, seam stretch elasticity, and pattern grading adjustments before fabric cutting.
From micro-encapsulated moisture management to ultrasonic seam bonding, explore the engineering breakthroughs defining modern athletic apparel performance.
Engineered body-mapping using specialized Italian Santoni seamless machines allows integrated breathability zones, targeted muscle compression, and zero chafing seams. Seamless construction minimizes fabric cutting waste by up to 35% compared to traditional cut-and-sew apparel.
Utilizing eco-friendly Italian Kian inks and industrial heat-transfer presses operating at 210°C, digital sublimation embeds color pigment directly into polyester micro-filaments. This ensures zero color fading, cracking, or peeling while maintaining complete fabric breathability under heavy sweat conditions.
Eliminating stitch holes entirely, high-performance waterproof outerwear and compression garments employ ultrasonic welding combined with thermo-adhesive polyurethane sealing tapes. This guarantees 10,000mm+ hydrostatic water protection and streamlined aerodynamic profiles.
Application of silver-ion biocides and phase-change materials (PCM) to yarn matrices inhibits odor-causing bacteria growth (Staphylococcus aureus) and regulates body core temperature during high-intensity marathon, cycling, and weightlifting activities.
Built upon three generations of manufacturing mastery in Sialkot, Pakistan, Haraka Sports delivers end-to-end OEM/ODM custom apparel solutions for global sports brands, clubs, and distributors.
Operating two dedicated production hubs (Daska Road Head Office and Small Industries Estate Unit), our facilities house computerized pattern grading, hydraulic cutting presses, chain-system stitching lines, and specialized sublimation labs under single-accountable management.
Every purchase order undergoes rigorous raw material quarantine, GSM weight validation, fabric shrinkage audits, needle-control metal detection, and final end-line AQL 2.5 statistical inspection before carton sealing.
From initial mood boards to custom woven neck labels, silicone heat-transfer logos, TPU hangtags, and custom artwork polybags—our design team converts your ideas into export-ready production Tech Packs. You retain total pattern ownership.
Incoming fabric lots are audited for color fastness, shade matching, shrinkage, and weight consistency against approved buyer swatches before room release.
Pattern markers are digitally optimized to maximize fabric yield. Panels are cut and bundle-numbered to prevent batch shade variation in assembly.
Specialized machine operators work on dedicated operations (flatlock, overlock, coverstitch) with hourly in-line roving inspection checks.
Garments are thread-trimmed, steam pressed for dimensional stability, and audited against graded size charts for measurement tolerance compliance.
Random unannounced inspections verify barcode tags, polybag art, carton markings, and stitching durability per military standard sampling plans.
Continuous sample development releases fit samples and sublimation strike-offs within 7–12 working days following technical specification clearance.
Essential guidance for global apparel buyers, brand directors, and procurement specialists seeking clarity on manufacturing logistics, MOQs, and customization.
Partner with a proven 3rd-generation OEM/ODM manufacturer. Request physical sample kits, fabric swatch books, or custom bulk pricing today.