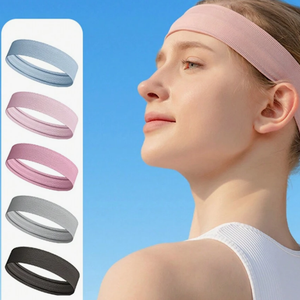
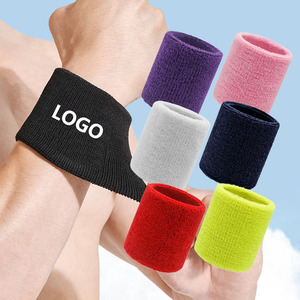
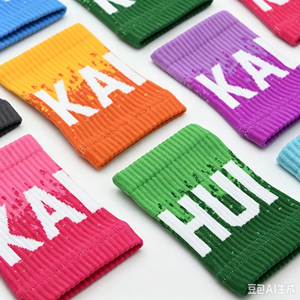
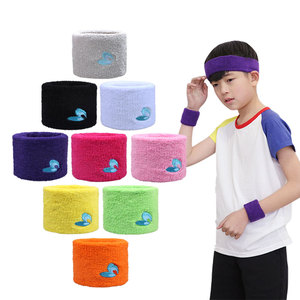
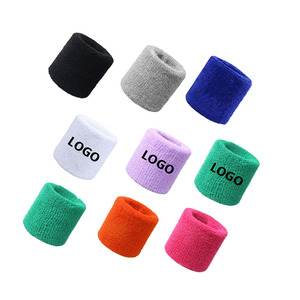
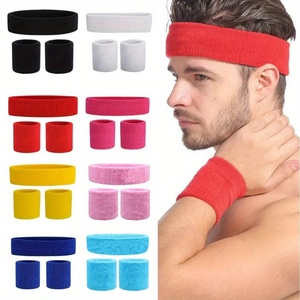
Engineered for high-sweat absorption, non-slip friction control, dynamic recovery, and private label branding. Explore our export-grade product line manufactured under audited quality standards.
An in-depth study on textile composition, moisture-wicking physics, fiber recovery, and sustainable sourcing strategies for athletic apparel procurement executives.
Modern athletic sweatbands have evolved beyond basic single-yarn cotton loops. Today’s high-performance sports wristbands and headbands rely on a carefully calibrated tri-blend matrix. By combining long-staple combed cotton (60–80%), high-tensile nylon (15–25%), and food-grade elastane (5–10%), manufacturers achieve optimal sweat absorption alongside dynamic elastic memory.
Combed cotton delivers soft skin contact and natural hydrophilic capillary action, absorbing up to 27 times its dry weight in aqueous fluids. Nylon provides structural stability against high-friction torque during intense workouts, while elastane prevents structural sagging after repeated wash cycles. Advanced OEM factories now incorporate phase-change micro-encapsulated yarns and bamboo-derived viscose to enhance thermoregulation and natural antimicrobial defenses.
The primary performance indicator of a commercial sweatband is its Moisture Transport Rate (MTR). Cheap sweatbands saturate quickly, becoming heavy, abrasive, and prone to slipping. Advanced technical sweatbands utilize dual-layer micro-channel knitting: the inner face against the skin features hydrophobic synthetic microfibers that pull liquid sweat away, while the outer face consists of high-surface-area hydrophilic loops that accelerate atmospheric evaporation.
Furthermore, non-slip headbands intended for running and yoga feature medical-grade, micro-injected wavy silicone grippers. Applied to the inner perimeter, these silicone wave patterns create friction against skin and hair without restricting cranial blood flow or pulling fine hairs.
Evaluating international production clusters based on yarn quality, OEM scalability, social compliance, and cost-efficiency.
When sourcing custom sweatbands, sports wristbands, and technical headwear, global procurement teams must balance unit costs against fabric consistency, lead-time reliability, and international compliance (e.g., Oeko-Tex Standard 100, BSCI, ISO 9001). Below is an analytical benchmark of the world's leading export hubs and top manufacturing partners.
| Manufacturing Hub / Region | Primary Specialties | Typical Lead Time | Core Advantage | Export Compliance |
|---|---|---|---|---|
| 1. Sialkot Hub (Haraka Sports - Pakistan) | Custom Terry Cloth, Sublimated & 3D Embroidered Sets | 25 - 40 Days | Vertical Integration, Flexible MOQs (50-150 pcs), 3rd Gen Mastery | ISO 9001, AQL 2.5, BSCI Audited |
| 2. Zhejiang Cluster (Yiwu/Ningbo, China) | Mass Market Poly-Spandex & Promotional Sweatbands | 15 - 30 Days | High Volume Scale, Ultra-Fast Automated Knitting | REACH, Oeko-Tex Standard 100 |
| 3. Guangdong Division (Dongguan, China) | Seamless Tech Headbands & Bonded Laser-Cut Bands | 20 - 35 Days | High-End Activewear Integration, Silicone Injection | ISO 14001, Sedex SMETA |
| 4. Tamil Nadu Hub (Tirupur, India) | 100% Organic Cotton Terry Wristbands & Knitted Gear | 30 - 45 Days | GOTS Organic Yarn Sourcing, Abundant Raw Cotton | GOTS Certified, WRAP |
| 5. Northern Region (Hanoi, Vietnam) | Synthetics, Seamless Athletic Accessories & Sports Bras | 30 - 50 Days | Competitive Tariff Structures for US & EU Markets | WRAP, BSCI Compliance |
| 6. Punjab Manufacturing Zone (Pakistan) | Heavyweight Heavy-Duty Powerlifting & Gym Wrist Wraps | 25 - 40 Days | High Tensile Elastic Fabrics & Custom Hardware Integration | ISO 9001 Quality Control |
| 7. Porto Industrial District (Portugal) | Premium European Boutique Activewear & Bamboo Headbands | 20 - 30 Days | Nearshoring for EU Luxury Brands, Zero Duty in EU | EU Reach, Oeko-Tex Class 1 |
| 8. Istanbul Textile Region (Turkey) | Cotton-Rich Athletic Socks, Sweatband Set Combos | 20 - 35 Days | Fast Freight to Western Europe, Superior Aegean Cotton | Sedex, Oeko-Tex Standard 100 |
| 9. Taichung Cluster (Taiwan) | High-Tech Moisture Wicking Yarns & Phase-Change Bands | 25 - 40 Days | Patented Cooling Yarns & Reflective Safety Prints | Bluesign Certified, ISO 9001 |
| 10. Sialkot Small Estate (Pakistan) | Multi-Sport Accessories, Leather & Nylon Gym Accessories | 20 - 35 Days | Consolidated Shipments with Apparel & Accessories | Custom Quality Protocols |

Combining three generations of textile mastery in Sialkot with modern lab testing, transparent supply chains, and low minimum development runs.
Haraka Sports operates two fully managed production facilities in Sialkot, Pakistan: our flagship facility at 8 km Daska Road and our second unit within the Small Industries Estate. Having two dedicated operations allows us to run specialized chain-system stitching lines for knit accessories simultaneously alongside cut-and-sew athletic apparel.
This dual-unit architecture ensures that custom terry cloth wristbands, sublimated basketball uniforms, and gym accessories can be processed together and consolidated into a single export carton, slashing freight expenditures for overseas buyers.
Quality control at Haraka Sports is not an afterthought—it is integrated into every step of raw material handling and assembly. Every single yarn lot entering our warehouse undergoes immediate quarantine testing. We measure GSM weight accuracy, dimensional shrinkage after washing, color fastness to rubbing and perspiration, and pilling resistance.
Our dedicated QC auditors enforce an AQL 2.5 standard across in-line roving checks and pre-shipment inspections. Non-conforming fabric rolls are immediately returned to the yarn mill rather than blended into bulk production runs.
We believe scalable growth requires supporting emerging activewear brands alongside established global distributors. While conventional textile mills demand tens of thousands of units per style, Haraka Sports supports development orders starting at just 50 to 150 pieces per style for custom sublimated and terry accessories.
Our in-house sample development room delivers physical fit samples, embroidery strike-offs, and customized polybag packaging artwork in just 7 to 12 working days post tech-pack signoff.
A transparent, documented trail ensuring zero defect tolerance from raw yarn delivery to sealed ocean containers.
Incoming cotton loops, polyester yarns, and elastane threads are tested for GSM weight tolerance, shade-band consistency against master lab dips, and rub fastness before release.
Patterns are digitally marker-planned for optimal yield. Hydraulic press cutters stamp precision panel shapes. Bundles are individually numbered by size to guarantee strict shade matching.
Workplace-specialized operators utilize high-speed circular terry knitting machinery, multi-head embroidery systems, flatlock seamers, and needle-detection safety protocols.
Garments and sweatbands pass through continuous steam irons for dimensional stabilization. Loose threads are manually trimmed, followed by 100% surface inspection for oil spots or skipped stitches.
Independent internal inspectors pull random samples from packed cartons. Measurements, barcode scannability, woven tag placement, and carton marking ratios are verified against the PO.
Every completed purchase order undergoes a post-production audit. Lessons learned are recorded into our permanent pattern and material library to continuously improve future runs.
Key technological shifts shaping activewear accessory procurement over the next decade.
Environmental regulations and consumer expectations are pushing activewear buyers toward circular materials. Leading exporters are replacing virgin polyester with GRS-certified (Global Recycled Standard) post-consumer rPET yarns derived from recycled ocean plastics and plastic bottles.
Simultaneously, organic combed cotton and bamboo-derived rayon are gaining market share in sweatbands due to their natural softness, biodegradable profile, and lower carbon footprint during cultivation.
Flat screen prints on flexible wristbands often crack after repeatedly stretching during use. Modern OEM buyers are transitioning to micro-injected 3D high-density silicone prints and direct jacquard weave structures.
Jacquard weaving integrates logo designs directly into the fabric's knitted core, guaranteeing that branding will never peel, fade, or crack, regardless of wash cycles or mechanical stress.
Clear answers to technical sourcing, ordering procedures, customization options, and international shipping protocols.
For custom knitted terry cloth wristbands and sublimated non-slip headbands, our standard production minimum starts at 50 to 150 pieces per style/colorway. For complex custom-dyed Pantone yarns or specialized jacquard weaves, MOQs typically range between 300 and 500 pieces, allowing brands to test new product lines with low inventory risk.
All raw cotton and synthetic yarns undergo rigorous lab testing under ISO 105-C06 (color fastness to washing) and ISO 105-E04 (color fastness to perspiration). We only use eco-friendly reactive dyes that chemical-bond with textile fibers, ensuring zero color transfer onto skin, uniforms, or athletic wear during intense perspiration.
Yes. Because Haraka Sports manufactures activewear, team sportswear, hoodies, tracksuits, and gym accessories across our two Sialkot facilities, we can consolidate all your SKUs into a single sea or air freight shipment. This significantly lowers customs clearing fees, container handling costs, and import documentation overhead.
We offer a comprehensive array of custom branding methods tailored to product functionality: 3D high-density thread embroidery, woven edge labels, direct jacquard pattern integration, heat-transfer silicone logos, reflective night-visibility prints, and micro-injected silicone grippers.
Once tech packs and artwork vector files are confirmed, pre-production physical samples and strike-offs are dispatched within 7 to 12 working days. Upon sample signoff and deposit receipt, bulk mass production takes between 25 and 40 days, depending on order complexity, custom dye requirements, and shipping mode.
Absolutely. We produce fully customized retail presentation options including FSC-certified recycled card hangtags, polybags printed with custom artwork and barcodes, bio-degradable frosted bags, and multi-piece retail display boxes suitable for e-commerce or brick-and-mortar retail environments.
Connect directly with Haraka Sports' engineering and merchandising team in Sialkot, Pakistan. Request physical fabric swatches, technical cost breakdowns, or custom sample developments today.