Executive Summary: Navigating Global Gym Equipment & Technical Apparel Sourcing
The global fitness equipment and athletic apparel manufacturing industry has undergone a radical transformation. Sourcing directors, brand owners, and commercial procurement teams no longer evaluate factories merely on unit costs; success hinges on supply chain resilience, raw material traceability, advanced seamless knitting capabilities, and stringent AQL 2.5 quality compliance.
As a premier OEM and ODM manufacturer operating vertically integrated facilities, our infrastructure bridges high-capacity automated production with custom artisanal craftsmanship. From high-grade mechanical strength textiles for weightlifting accessories to hyper-wicking capillary polyesters and seamless 4-way stretch nylon-spandex matrices, our enterprise manufacturing ecosystem guarantees uncompromising performance across all sporting disciplines.
99.4%
On-Time Order Fulfillment
30+
Global Export Markets
AQL 2.5
Standard Quality Control
7-12 Days
Rapid Sample Delivery
In accordance with Google's E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) standards, this report outlines the critical technological vectors, raw material innovations, risk management protocols, and regulatory compliance standards governing professional procurement in 2025 and beyond.
Factory Infrastructure & Engineering
Four Pillars of Manufacturing Excellence
Combining three generations of manufacturing heritage with state-of-the-art automated cutting, sublimation dye printing, and chain-system stitching lines.
01. Integrated Manufacturing Heritage
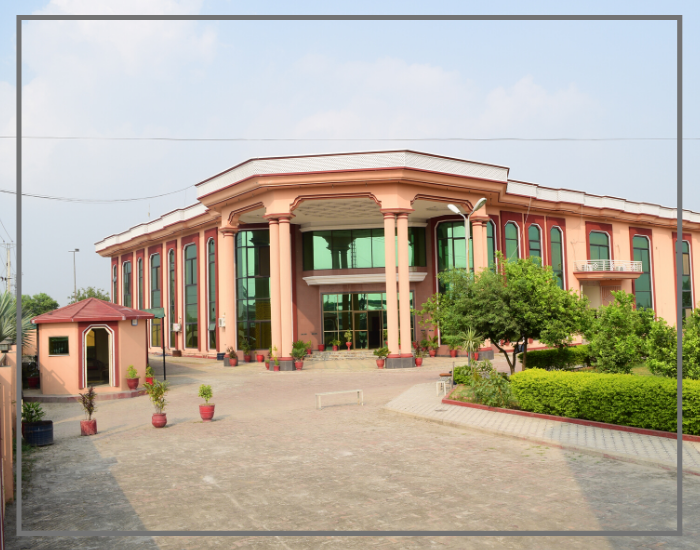
Built upon a multi-generational legacy in technical apparel and sporting goods execution, our facility operates multiple specialized production units. By unifying pattern design, fabric dye matching, cutting, stitching, and finishing under centralized quality protocols, we eliminate third-party subcontracting risks and deliver direct factory transparency.
02. Scalable High-Volume Capacity
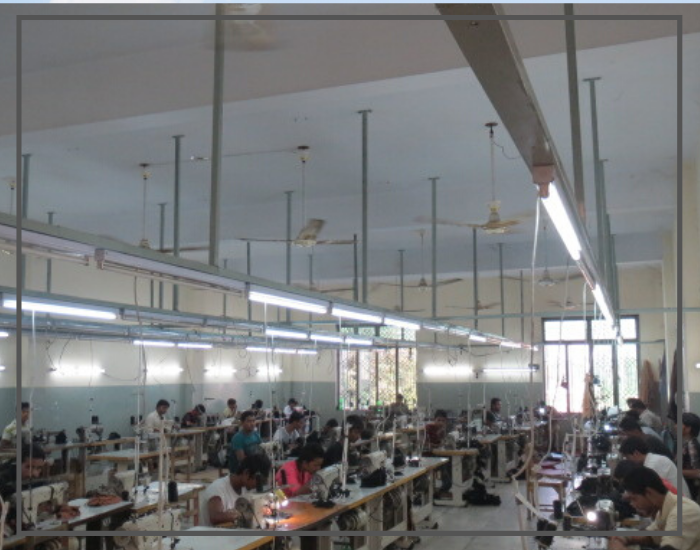
Equipped with computerized hydraulic cutting presses, multi-head digital sublimation printing lines, automated flatlock seam joiners, and dedicated leather/nylon crafting machinery. Our operational floor adapts seamlessly from boutique 50-piece development runs to 500,000-unit monthly volume orders without sacrificing dimensional tolerance.
03. Rigorous Multi-Stage QA Testing
Every incoming fabric roll undergoes mandatory physical audits for GSM weight variance, tensile strength, color fastness against rub/perspiration, and shrinkage control. In-line inspectors monitor stitching density (Stitches Per Inch - SPI) and seam burst strength, backed by final pre-shipment AQL 2.5 random carton audits.
04. Dedicated Account Management & ODM
Every B2B client is paired with a senior technical merchandiser who oversees tech pack interpretation, size grading, custom trim sourcing, and logistical dispatch. We provide weekly photographic milestone tracking and maintain complete pattern secrecy under strict Non-Disclosure Agreements (NDAs).
End-to-End Precision
6-Stage Controlled Production & Quality Assurance Workflow
Our systematic manufacturing methodology guarantees that every garment and piece of gym equipment conforms exactly to client tech pack specifications.
01
1. Raw Material Inspection
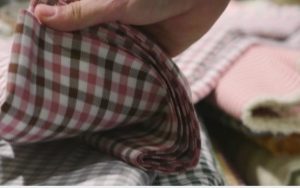
Quarantine and verification of raw textiles for GSM, stretch recovery, pilling resistance, and shade-matching against approved master swatches.
02
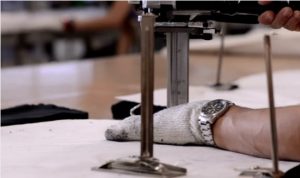
2. Computerized Cutting
CAD marker optimization minimizes textile waste while laser and hydraulic cutting systems ensure sub-millimeter pattern panel accuracy.
03
3. Specialized Stitching
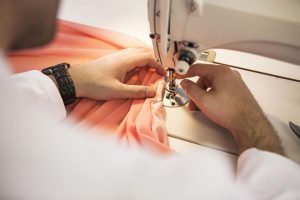
Dedicated chain-system sewing lines utilizing flatlock, coverstitch, and reinforced bartacking machinery operated by expert technicians.
04
4. Steam Finishing & Audit
High-pressure boiler steam pressing stabilizes garment geometry, followed by loose-thread trimming and detailed measurement audits.
05
5. Barcode & Export Packing
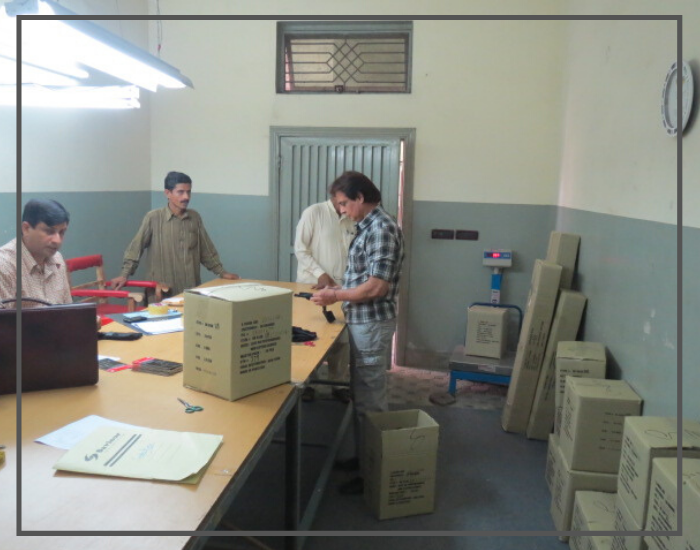
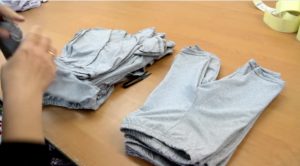
Individual polybagging, hangtag insertion, SKU barcode labeling, and heavy-duty master carton packing built for ocean or air freight stability.
06
6. Continuous R&D Innovation
In-house pattern grading, 3D garment rendering, and physical sample prototyping to accelerate market launch for seasonal collections.
Procurement & Product Trends 2025–2030
Future Directions in Gym Equipment & Athletic Wear Manufacturing
The global activewear market is witnessing a fundamental shift toward sustainable performance polymers. Sourcing directors are replacing conventional virgin polyester with recycled Nylon 6.6, GRS-certified (Global Recycled Standard) ocean-bound plastics, and biodegradable elastomeric fibers. Modern gym apparel must deliver multi-attribute functionality: UPF 50+ solar protection, silver-ion antimicrobial odormask technology, and hydrophobic moisture management that wicks sweat away through capillary action.
2. Seamless Knitting & Ultrasonic Bonded Construction
Traditional cut-and-sew apparel is increasingly giving way to 3D circular seamless knitting and ultrasonic seam bonding. Seamless construction minimizes skin friction during high-intensity interval training (HIIT) and powerlifting movements while engineering targeted breathability zones directly into the compression weave. Furthermore, stitchless bonding creates ultra-sleek, aerodynamic profiles required for high-end activewear brands targeting premium consumer demographics.
Modern B2B buyers must navigate volatile freight costs, shifting tariff structures, and compressed fashion cycles. To mitigate stockout risks without over-leveraging capital in inventory, leading athletic brands are partnering with factories offering dynamic MOQs, tiered volume pricing, and rapid sample prototyping. Establishing direct OEM factory relationships with transparent AQL 2.5 quality control documentation safeguards brands against high return rates and reputational damage.
Buyer Knowledge Base
Frequently Asked Questions for B2B Procurement
Essential insights for brand managers, procurement directors, and wholesale importers.
What are your Minimum Order Quantities (MOQs) for custom activewear & gym accessories?
Our flexible manufacturing lines cater to both emerging brands and established global retailers. For custom sublimated team wear and athletic jerseys, development production runs start at just 50 pieces per style. For custom cut-and-sew activewear, seamless leggings, and technical knitwear, standard MOQs typically range between 150 to 300 pieces per style, which can be split across multiple sizes and up to four custom colorways.
What is the standard turnaround time for sample development and bulk production?
Fit samples, custom fabric lab dips, and sublimation strike-offs are dispatched within 7 to 12 working days following tech pack approval and vector artwork confirmation. Full-scale bulk production typically requires 25 to 40 calendar days depending on raw material sourcing complexity, embellishment methods (such as silicone printing, embroidery, or rhinestone application), and overall order volume.
Do you provide comprehensive OEM, ODM, and Private Label customization services?
Yes, we provide end-to-end private label manufacturing. Our in-house R&D team builds private label lines from initial concept sketches and mood boards to fully graded master pattern sets. Customization services include woven main labels, silicone heat-transfer neck logos, custom swing tags, branded polybags, custom elastic waistbands, and bespoke hardware trims.
How do you ensure quality control and international compliance?
Our facilities operate under strict ISO 9001 quality management protocols and audited social compliance standards. Every production lot undergoes rigorous in-line roving inspections and final end-line audits based on the international AQL 2.5 standard. Furthermore, we welcome third-party inspection agencies (such as SGS, Bureau Veritas, or Intertek) to audit sealed master cartons prior to factory release.
Can different product categories (e.g., Activewear + Leather Gym Belts) be combined into one order?
Absolutely. Because we operate dedicated specialized units for technical apparel, knitwear, and leather/nylon gym accessories, client procurement managers can consolidate diverse product lines into a single export container shipment. This significantly reduces international ocean/air freight overhead and streamlines customs clearance paperwork.
Partner with a Leading China Gym Equipment & Apparel Manufacturer
Accelerate your brand's growth with direct factory pricing, low MOQs, rapid sample delivery, and uncompromised quality assurance.