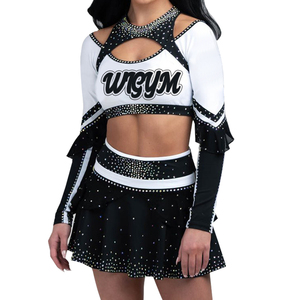
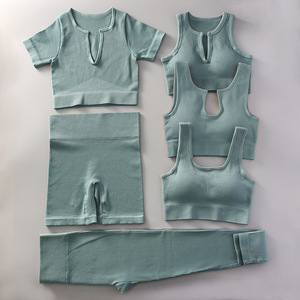
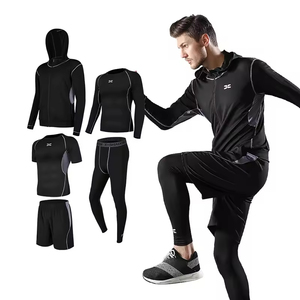
The global technical apparel market is undergoing a seismic structural pivot. No longer driven solely by price-per-unit cost matrices, international activewear brands, sportswear wholesalers, and boutique fitness labels are evaluating apparel manufacturers based on technical execution speed, material innovation depth, and supply chain transparency. China remains the undisputed global nexus for high-performance apparel manufacturing, producing over 55% of the world’s synthetic functional textiles and seamless sports garments.
The strategic strength of China’s performance apparel exporters lies in hyper-clustered industrial hubs. From functional yarn extrusion and circular warp knitting in Zhejiang and Fujian to high-precision seam-bonding, 4-needle 6-thread flatlock assembly, and sublimation printing in Guangdong and key partner facilities, the end-to-end integration dramatically minimizes supply chain lead times. Purchasing decision-makers who partner with vertically integrated manufacturers secure significant information and margin advantages over competitors relying on fragmented supply networks.
Strategic Information Gain for Sourcing Managers: Modern performance apparel sourcing requires evaluating suppliers on four core criteria: yarn extrusion capabilities (e.g., bio-based polyesters and recycled nylon 6,6), circular knitting density (gauge consistency), automated bonding/cutting precision, and third-party audited environmental compliance (OEKO-TEX Standard 100, GRS, and HIGG Index).
Analyzing the functional fabric innovations shaping global athletic and lifestyle performance apparel markets.
1. High-Gauge Seamless Circular Knitting
Seamless technology utilizes specialized SANTONI circular knitting machines to engineer target compression zones directly into the garment structure without traditional cut-and-sew seams. This reduces fabric waste by up to 30% while eliminating skin chafing during high-intensity training. Blends of microfiber nylon and Elastane provide optimal recovery, opacity, and body-contouring fits.
2. Smart Moisture Management & Thermoregulation
Next-generation polyester interlocks feature cross-section yarn channels (such as star or cross shapes) that create capillary action. Moisture is instantly drawn away from the skin surface and spread across an expanded outer evaporation layer. Hydrophilic fast-dry coatings combined with anti-bacterial silver-ion treatments ensure odor control and thermal stability across dynamic climate conditions.
3. Bonded Seams & Ultrasonic Construction
To achieve ultra-lightweight aerodynamic designs for marathon vests, cycling jerseys, and weather-proof outerwear, premium manufacturers utilize hot-melt adhesive tapes and ultrasonic seam welding. This stitchless assembly eliminates needle punctures, ensuring 100% water resistance while reducing overall garment weight by up to 20% compared to traditional stitching.
Environmental compliance is no longer optional. Leading exporters offer fully traceable Recycled Polyethylene Terephthalate (rPET) derived from post-consumer plastic bottles, certified under the Global Recycled Standard (GRS). Closed-loop waterless dye processes reduce chemical usage and wastewater discharge by up to 80% while retaining color fastness grade 4.5+.
Future Procurement Trends in Global Apparel Sourcing
• Digital Twin Prototyping & 3D Design
Global brands are replacing physical sampling iterations with 3D CAD simulation platforms like CLO3D and Optitex. Exporters with dedicated 3D pattern rooms deliver virtual fit samples within 48 hours, reducing sample waste by 75% and accelerating time-to-market by 3 to 4 weeks.
• Low-MOQ Agile Supply Chains
The shift toward flexible inventory models has forced manufacturers to restructure production lines. Leading facilities now accept tiered MOQs starting from 50–150 pieces per style for sublimated team wear and specialized cut-and-sew programs, enabling rapid market testing without heavy capital lockup.
• Full Supply Chain Transparency & ESG Audits
Importers in the EU and North America require complete material traceability down to the raw polymer level. Exporters maintaining digital chain-of-custody documentation, BSCI social compliance certifications, and zero-discharge water treatment lead the premium OEM sector.
Enterprise Advantage & Quality Control Pipeline
Combining three generations of manufacturing heritage with strict AQL 2.5 inspection protocols across 6 integrated production stages.
01
Material & GSM Testing
Every incoming fabric lot undergoes rigorous lab testing for GSM weight accuracy, dimensional shrinkage, color fastness, anti-pilling rating, and stretch elasticity before release to the cutting floor.
02
Precision Cutting & Bundling
Automated markers and hydraulic die-cutting presses ensure millimetric panel accuracy. Panel-level inspections and size bundling prevent shade variation across bulk lots.
Garments pass through high-pressure boiler steam pressing for structural stabilization. Thread trimming and meticulous hand audits remove non-conforming items prior to tagging.
05
AQL 2.5 Pre-Shipment Audit
Random unannounced sampling of sealed cartons verifies polybag barcoding, assortment ratios, hangtags, and metal detection compliance under strict AQL 2.5 acceptance criteria.
06
Full ODM R&D & Tech Packs
In-house design engineers convert mood boards into graded tech packs, custom trim specs, heat-transfer artwork, and physical fit prototypes in 7–12 working days.
Why Global Brands Partner With Our Manufacturing Hubs
Combining specialized manufacturing hubs in China with international export partnerships (including third-generation heritage operations in Sialkot), our enterprise delivers an unmatched multi-category OEM/ODM sourcing framework. Buyers can consolidate diverse product categories—including sublimated sports kits, high-compression seamless activewear, brushed fleece knitwear, waterproof softshell outerwear, and leather/nylon fitness accessories—into a single synchronized export shipment.
Dedicated Account Merchandising
Every client is paired with a dedicated English-speaking apparel merchandiser who provides weekly video/photo production updates across cutting, stitching, and finishing milestones.
Complete Private Label Customization
From custom woven neck labels and high-density silicone chest prints to anti-counterfeit QR polybags and branded hangtags, we execute end-to-end brand identity packages.
Frequently Asked Sourcing & Procurement FAQs
Essential guidance for purchasing agents, brand directors, and apparel buyers sourcing from China manufacturers.
What is the typical Minimum Order Quantity (MOQ) for custom technical apparel?
For fully sublimated team wear (such as basketball uniforms, soccer kits, and cycling jerseys), our MOQs start as low as 50 pieces per style. For cut-and-sew activewear, seamless yoga sets, and cotton knitwear programs, our standard MOQ is 150 to 300 pieces per style, which can be split across multiple sizes and up to 3–4 colorways.
What are the timelines for sampling, rapid prototyping, and bulk production?
Fit samples, digital sublimation strike-offs, and fabric swatches are produced and dispatched within 7 to 12 working days following tech pack confirmation. Bulk production lead time typically ranges from 25 to 40 calendar days, depending on fabric mill development, embellishment complexity, and overall order quantity. Repeat re-orders on approved patterns follow an expedited schedule.
Do you provide complete ODM private label collection development?
Yes. Our full-service ODM engineering room builds private label apparel lines from basic concept sketches or mood boards down to graded size charts and tech packs. We handle custom trim sourcing, rubber/silicone heat transfers, woven neck labels, custom polybag packaging, and barcoding. All pattern rights remain 100% exclusive to the client.
How do you guarantee quality control and international compliance?
We enforce strict AQL 2.5 (Acceptable Quality Limit) standards for inline and final pre-shipment inspections. Every fabric lot is tested for weight (GSM), shrinkage variance, color fastness to washing/rubbing, and pilling resistance. Our partner facilities operate under BSCI, OEKO-TEX Standard 100, and ISO 9001 certifications. Third-party inspection agencies (SGS, TUV, ITS) are welcome at any stage.
Can we consolidate activewear, sportswear, and fitness accessories into one container?
Absolutely. Because our integrated manufacturing capabilities encompass apparel stitching lines, seamless knitting units, and specialized accessory production (such as weightlifting gloves, belts, and gym wraps), we consolidate multi-category orders into single sea or air freight shipments, significantly lowering landing costs and import customs overhead.