1. Strategic Supply Chain Blueprint: China Teamwear Manufacturing Ecosystem
As global sports brands, collegiate athletic departments, professional clubs, and private-label distributors scale their apparel lines, the demand for verified, technically competent teamwear manufacturing partners has reached an unprecedented high. Procurement managers no longer evaluate factories purely on unit FOB pricing. Instead, global purchasing decisions in 2025 are driven by Information Gain, supply chain resilience, advanced yarn science, certified environmental compliance, and digital pattern precision.
China's teamwear manufacturing landscape has undergone a profound technological transformation. Traditional labor-intensive assembly lines have given way to smart cut-and-sew units integrated with automated laser cutters, digital CAD grading systems, and high-precision Italian dye-sublimation machinery. By maintaining localized supply ecosystems—ranging from recycled polymer extrusion mills in Zhejiang to specialized trimming and embroidery hubs—China remains the undisputed benchmark for high-performance activewear and custom teamwear production.
Technical Insight: High-performance teamwear requires exact fabric tension control and thermal stabilization during sublimation. Our automated tensioning systems maintain yarn stretch memory, ensuring zero distortion during high-heat transfer processes.
Material Engineering & High-Performance Synthetic Fabrics
Modern athletic competition demands specialized textile engineering tailored to sport-specific bio-mechanics. As a top-tier China OEM/ODM manufacturer, our R&D facilities focus on four core yarn matrix configurations:
Micro-Filament Moisture Management Polyesters: Utilizing cross-section channel fibers (such as Coolmax-type structures) that create capillary action, pulling sweat away from the dermis to the outer fabric layer for rapid evaporation.
High-Gauge Elastomeric Fabrics (Nylon/Spandex Blends): Engineered with 18% to 30% elastane for compression garments, sports bras, and cheerleading uniforms, providing dynamic muscular support and reducing lactic acid buildup without restricting full range of motion.
Recycled PET Yarns (GRS-Certified): Post-consumer plastic bottle polyester, offering identical tensile strength, colorfastness, and abrasion resistance while satisfying strict corporate ESG standards.
UPF 50+ UV-Blocking & Antimicrobial Coatings: Inorganic titanium dioxide yarn integration combined with eco-friendly silver-ion surface treatments, offering durable protection against solar radiation and bacterial odor retention across 50+ industrial wash cycles.
Operational Excellence
Factory Pillars & OEM/ODM Capabilities
Combining multi-generational textile mastery with modern quality management systems for seamless international production execution.
Pillar 01
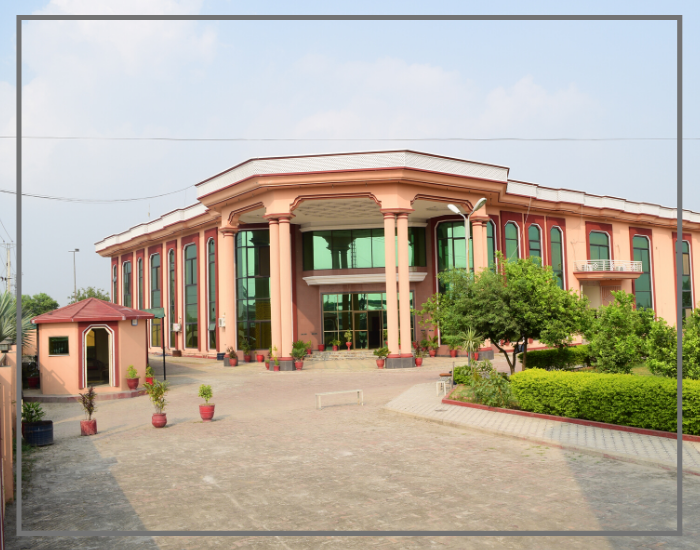
Enterprise Infrastructure
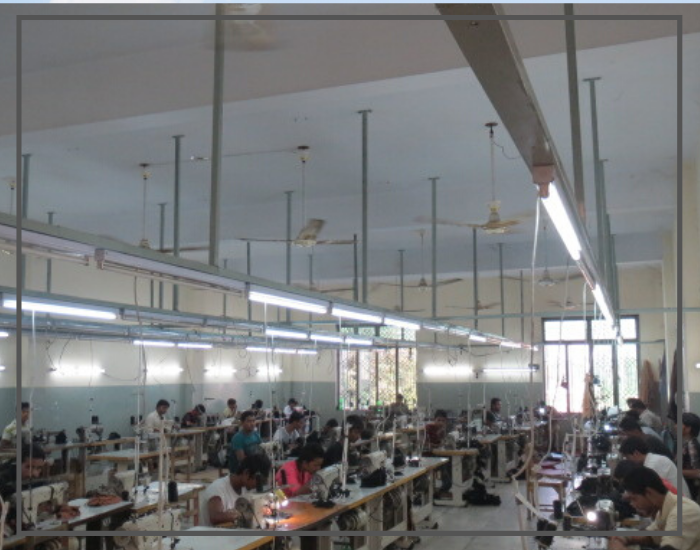
State-of-the-art facility equipped with specialized chain-stitching lines, hydraulic cutting presses, and eco-friendly printing units designed for high-capacity batch orders.
Pillar 02
Scalable Capacity
Parallel production lines flexible enough to execute low-MOQ custom team runs (from 50 pcs) alongside high-volume seasonal retail collections without bottlenecks.
Pillar 03
AQL 2.5 Quality Control
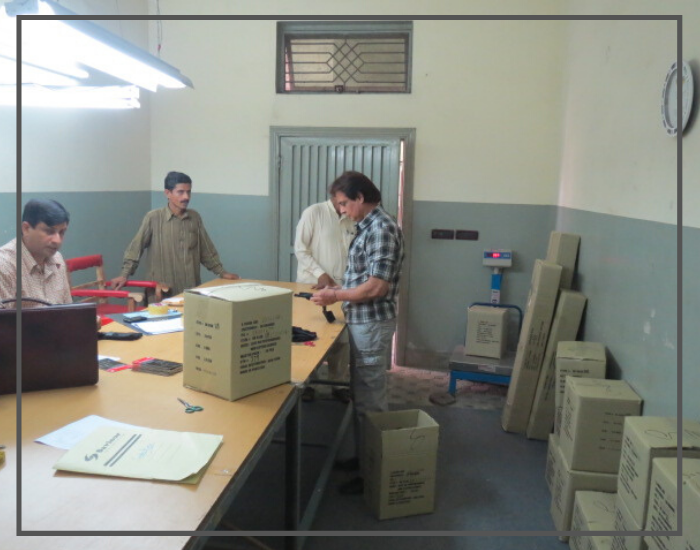
Rigorous incoming raw fabric audits, inline roving inspections, needle-detector screenings, and final pre-shipment AQL 2.5 defect tracking for zero-fault delivery.
Pillar 04
Dedicated Account Managers
Direct bi-lingual merchandising leads handling technical tech packs, digital 3D apparel mockups, weekly milestone tracking, and seamless export logistics handling.
2. Global Sourcing Analysis: Future Teamwear Procurement Trends (2025–2030)
As international supply chains evolve, teamwear buyers must adapt to dynamic consumer expectations and shift away from rigid legacy procurement frameworks. Based on market intelligence gathered across European and North American sporting goods channels, four macro trends will define teamwear manufacturing over the next decade:
1. On-Demand Micro-Customization & Low MOQs
Distributors are drastically cutting inventory holding risks. The industry standard is shifting toward micro-batch ordering with rapid replenishment cycles. Advanced digital sublimation setups enable single-team customization at bulk cost structures.
2. Smart Fabrics & Ergonomic Zoning
High-performance jerseys now integrate body-mapped ventilation panels created via laser perforation and engineered jacquard knits. Target heat zones feature lower GSM mesh, while contact zones utilize high-denier anti-abrasion yarns.
3. Circular Economy & Mono-Material Design
Strict European eco-regulations mandate recyclable garment construction. Future teamwear relies heavily on mono-material designs (100% recyclable polyesters including trims and threads), allowing end-of-life garments to enter closed-loop re-polymerization.
Dye-Sublimation Technology vs. Traditional Decoration Methods
In high-contact sports such as cheerleading, basketball, soccer, and triathlon racing, screen printing and heavy vinyl transfers present significant drawbacks—including cracking, peeling, breathability blockage, and added weight. Full Italian ink dye-sublimation fuses non-toxic disperse dyes directly into the molecular structure of synthetic fibers under 200°C heat and pressure. The resulting print becomes an indelible part of the fabric, yielding ultra-vibrant colors (matching Pantone PMS systems with 99% accuracy) while maintaining 100% of the fabric's original breathability and stretch.
Specialized Production Lines
Five Core Apparel Manufacturing Divisions
Each division operates specialized sewing equipment, dedicated pattern rooms, and independent quality checking tables tailored to specific garment structures.
Sportswear
Sublimated basketball, soccer, cycling, and running kits engineered with reinforced flatlock seams.
Activewear
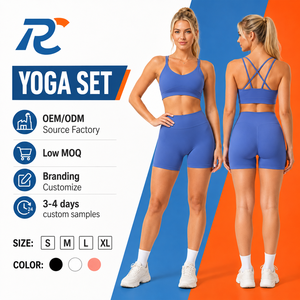
Four-way stretch gym sets, high-waist yoga leggings, and high-impact sports bras for fitness lines.
Knitwear
Heavyweight French terry hoodies, cotton-blend sweatpants, henleys, and casual team travel suits.
Outerwear
Windbreakers, softshell team jackets, and seam-taped waterproof rain shells built for harsh weather.
To eliminate production variance and deliver consistent quality across bulk runs, our factory operates under a standardized 6-stage Quality Assurance framework. Every single purchase order is tracked via dedicated internal ERP routing sheets.
01
Raw Material Inspection
100% incoming fabric inspection measuring exact GSM weight, roll width, color fastness (wash/rub test Grade 4.5+), and shrinkage parameters before fabric release.
02
CAD Patterning & Laser Cutting
Computerized marker efficiency optimization combined with precision laser cutting ensures perfect dimensional accuracy across all size gradings (XS to 5XL).
03
Digital Sublimation & Printing
High-resolution Japanese Mimaki digital printers using premium non-fading Italian inks deliver exact Pantone-matched graphics at 720x1440 DPI fidelity.
04
Ergonomic Assembly & Stitching
Specialized chain-system sewing lines employing 4-needle 6-thread flatlock machines, heavy-duty bartacking, and silicone elastic band bonding.
05
Steam Pressing & Inline Inspection
Boiler steam iron pressing to fix final garment silhouette, followed by 100% thread trimming, seam pull testing, and inline workmanship auditing.
06
AQL 2.5 Pre-Shipment Audit
Final random sampling audit covering custom hangtags, woven main labels, SKU barcode accuracy, metal detection, and waterproof polybag carton packing.
Buyer Intelligence
Frequently Asked Questions (FAQ) for Global Buyers
Clear, direct answers regarding custom teamwear sampling, manufacturing lead times, MOQs, quality standards, and private label ODM branding.
What is the Minimum Order Quantity (MOQ) for custom teamwear and activewear?
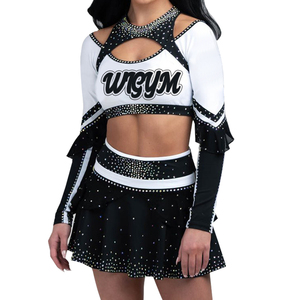
For full-sublimation sports uniforms (such as cheerleading outfits, basketball kits, soccer jerseys, and marathon singlets), our minimum order quantity starts at just 50 pieces per style/design with flexible size distribution. For cut-and-sew activewear, hoodies, and seam-taped outerwear, typical minimum development runs start at 100 to 150 pieces per colorway.
What are your turnaround times for sample development and bulk mass production?
Pre-production fit samples and color print strike-offs are completed and dispatched via express air courier within 7 to 12 working days after tech pack or vector art approval. Bulk mass production lead times typically range from 20 to 35 calendar days depending on fabric knitting development, embellishment complexity, and total order volume.
Do you offer complete ODM private label development and custom branding packaging?
Yes. We provide comprehensive OEM/ODM private-label solutions. Our technical design room works directly from your sketches, mood boards, or reference samples to build full graded tech packs. OEM branding services include custom heat-transfer neck labels, high-density woven main labels, silicone rubber badges, custom embossed hangtags, eco-friendly frosted zip-lock polybags, and barcode sticker integration.
How does your factory guarantee color accuracy and fabric quality consistency?
We utilize the global Pantone Matching System (PMS Solid Coated) to verify all print artwork. Digital color strike-offs are evaluated under standardized D65 light boxes. For raw materials, every fabric lot undergoes laboratory testing for gram weight (GSM variance within ±3%), dimensional wash stability (shrinkage under 3%), color fastness against washing and perspiration (Grade 4.5+), and pilling resistance before cutting.
Can we consolidate different product types (e.g., jerseys, hoodies, gloves) in one shipment?
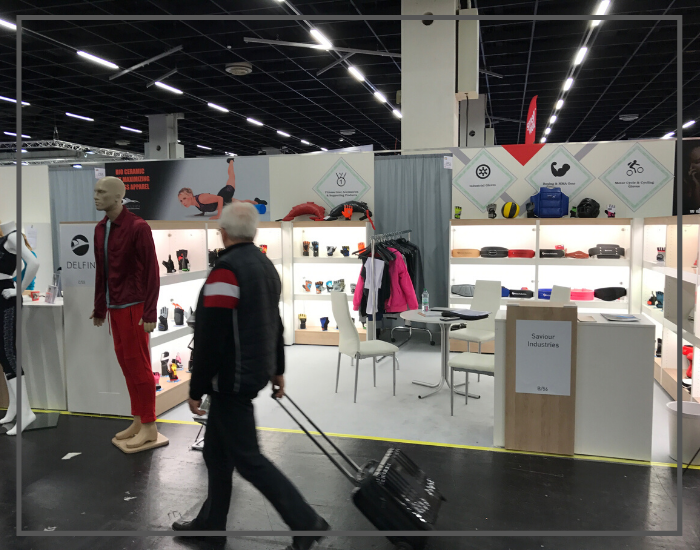
Absolutely. Because our facility operates specialized production units for sublimated teamwear, activewear, cut-and-sew fleece knitwear, waterproof outerwear, and leather fitness accessories under one corporate umbrella, all items can be consolidated into a single sea or air freight shipment. This significantly lowers freight costs, customs clearance fees, and logistical complexity.
Ready to Scale Your Teamwear Brand with China's Premier Factory?
Partner directly with an established OEM/ODM manufacturer. Request our comprehensive product catalog, fabric swatch books, and wholesale price quotes today.