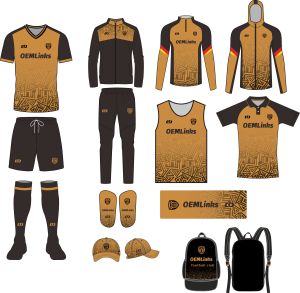
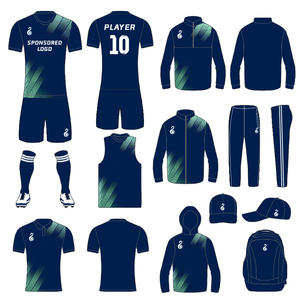
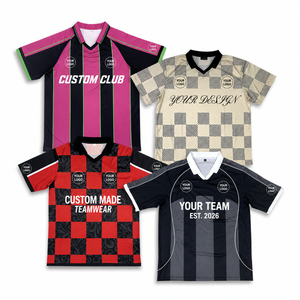
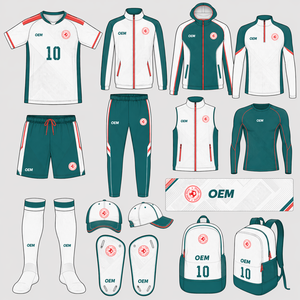
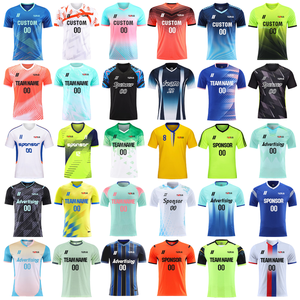
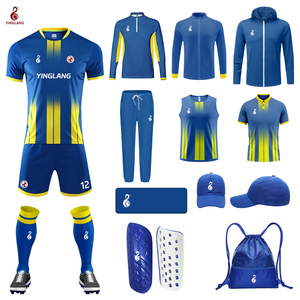
Engineered for professional leagues, retail apparel brands, and wholesale distributors. Explore our core OEM/ODM football uniform categories.
Three generations of apparel manufacturing excellence operating from Sialkot, Pakistan's global hub for technical sports gear production.
In the rapidly evolving global sportswear landscape, choosing a reliable football kits manufacturer and supplier requires more than evaluating unit costs. Sourcing executives, brand managers, and club procurement teams must navigate complex choices regarding technical fabric GSM weights, dye sublimation longevity, ergonomic pattern engineering, and social compliance standards. As a vertically integrated manufacturer operating out of Sialkot, Pakistan, Haraka Sports delivers end-to-end OEM and ODM capabilities engineered to satisfy the rigorous performance criteria of international sporting goods brands.
Technical specifications differ significantly between elite matchday kits ("Player Version") and retail fan merchandise ("Replica Version"). Understanding these material distinctions is crucial for optimizing your brand's margin structure and product positioning.
| Technical Parameter | Elite Player-Version Kit | Retail Fan (Replica) Kit | Training & Academy Kit |
|---|---|---|---|
| Fabric Composition | 88% Micro-Polyester / 12% Spandex Blend | 100% Recycled Interlock Polyester (rPET) | 100% High-Tenacity Birdseye Mesh |
| GSM Weight Range | 130 – 145 GSM (Ultra-Lightweight) | 160 – 180 GSM (Durable Structural Build) | 150 – 165 GSM (High-Abrasion Resistance) |
| Moisture Management | Capillary-Action Hydrophilic Finish | Standard Quick-Dry Moisture Wicking | Dual-Surface Ventilation Weave |
| Branding Embellishment | Heat-Applied 3D TPU Badges & Laser Edges | High-Density Woven Crests & Embroidery | Direct-to-Fabric Sublimation Printing |
| Seam Construction | Ultrasonic Bonded Seams / Flatlock Stitch | Reinforced 4-Thread Overlock Stitch | Heavy-Duty Double-Needle Coverstitch |
Dye-sublimation printing forms the backbone of modern customized teamwear. Unlike conventional screen printing, which deposits a physical layer of ink on top of the textile, digital sublimation converts dispersible dye inks directly into a gaseous state under precise temperature (200°C–215°C) and pressure parameters. The ink molecules bind directly into the micro-polyester polymer matrix, ensuring zero degradation of breathability or tactile flexibility.
At Haraka Sports, we utilize premium Italian Kian™ sublimation inks paired with Japanese Mimaki™ high-resolution print heads. This setup achieves a Pantone™ matching accuracy exceeding 98% and delivers a ISO 105-B02 color fastness rating of Grade 4.5+ against washing, perspiration, and intense UV exposure.
Sublimated graphics will never crack, peel, or fade, even after 100+ commercial laundry cycles under standard athletic wash protocols.
Computer-graded CAD pattern libraries modeled after international body sizing standards across North American, European, and Asian fits.
GRS-certified post-consumer recycled polyester options available, enabling eco-friendly product lines for sustainable brands.

Anticipating shifts in technology, environmental mandates, and supply chain logistics for high-volume apparel buyers.
Traditional physical sampling rounds consume 3 to 5 weeks and incur significant air-freight costs. The industry standard is rapidly transitioning toward 3D digital pattern software (CLO3D / Browzwear). At Haraka Sports, we provide high-fidelity 3D digital sample renderings within 48 hours of tech-pack submission, allowing buyers to verify drape, seam tension, and sublimated art scaling prior to physical sample cutting.
Regulatory shifts in the European Union and North America are making recycled textile content mandatory. Modern football kits are turning toward Global Recycled Standard (GRS) certified yarns produced from ocean-bound PET bottles. These yarns replicate virgin polyester's tensile strength, moisture management, and dye absorption while reducing carbon emissions by up to 35% per garment produced.
Stitchless jersey construction utilizing heat-bonded tapes and ultrasonic cutting is moving from elite professional kits into standard commercial teamwear collections. Seamless construction minimizes skin friction for athletes while reducing garment weight by 15%, providing a sleeker, modern aesthetic preferred by competitive clubs.
Wholesalers and teamwear brands are moving away from massive seasonal inventory builds, favoring flexible low-MOQ re-order models. Operating dedicated 50-piece development runs alongside automated high-volume chain lines allows sports brands to scale production dynamically based on real-time sales data.
Documented quality assurance executed per purchase order under strict AQL 2.5 inspection thresholds.
Incoming knit fabrics are tested for GSM consistency, shrinkage tolerance (<3%), pilling resistance, and shade-band uniformity before cutting authorization.
Automated marker planning maximizes fabric efficiency. Hydraulic press cutters and laser tables ensure cut-panel dimensional precision against graded spec sheets.
Transfers are heat-calibrated on industrial flatbed presses. Colors are verified against physical Pantone TCX standards under D65 daylight inspection lamps.
Specialized operators execute single-operation assembly on flatlock and coverstitch machinery. Roving QC inspectors audit stitch per inch (SPI) consistency hourly.
Garments undergo boiler steam pressing on modern buck forms. Thread trimming, badge inspection, and initial measurement audits occur at this stage.
Pre-shipment audit testing barcode accuracy, polybag sealing, carton drop-strength, metal-detection clearance, and final packing ratio verification.
Built on long-term commercial partnerships, technical transparency, and verifiable factory audit standards.
While standard cut-and-sew lines require 150–300 pieces per style, our sublimated teamwear department accepts orders starting from just 50 pieces per style, enabling fast testing of new market collections.
Eliminate middle-man trading fees. By contracting directly with our Sialkot manufacturing facilities, buyers achieve a 18% to 25% cost saving while gaining direct access to our engineering team.
From custom woven neck labels and heat-transfer sizing prints to custom polybags, hangtags, and branded carton sealing tapes, we deliver fully finished retail-ready products.
Clear answers to common B2B procurement queries regarding custom football kit manufacturing.
Partner directly with a third-generation Sialkot manufacturer. Request our comprehensive 2026 digital product catalog, physical swatch books, or a custom OEM quotation today.