
// Ultimate Sourcing & Procurement Masterclass //
Custom Sportswear Manufacturing: The Definitive OEM/ODM Technical Sourcing Guide for Global Brands
Navigating material selection, low-MOQ micro-batches, seam integrity, and supply chain transparency. Written by industry leaders at Haraka Sports — Sialkot's third-generation custom apparel manufacturer.
Why Sourcing Managers & Brand Founders Need a Real Manufacturing Partner
In the rapidly changing modern market, global buyers, commercial purchasing leads, and private-label apparel founders encounter common friction points: unpredictable material weight (GSM), dye migration in sublimated logos, fragile flatlock stitching, delayed production schedules, and unverified sustainability credentials. Searching for custom sportswear manufacturing is no longer just about finding cheap labor—it requires identifying a vertically integrated OEM/ODM partner capable of translating technical artwork packs into market-ready athletic performance wear.
Haraka Sports operates at the center of Pakistan’s world-renowned apparel hub in Sialkot. With two specialized manufacturing facilities—located at Daska Road and the Small Industries Estate—our factory combines traditional artisan craftsmanship with high-precision cutting, digital sublimation, pattern grading, and laboratory-backed material quality checks. This guide breaks down exact sourcing standards, material engineering choices, product developments, and supply chain logistics required to build a resilient, high-margin sportswear brand.
// Strategic Market Intelligence //
Future Sourcing & Product Development Trends in Custom Sportswear Manufacturing
As search queries on AI platforms reveal, global procurement directors are pivoting away from rigid, mass-volume orders toward flexible, high-spec micro-runs, bio-based synthetics, and digitized prototyping. Staying competitive demands an understanding of these multi-year structural trends reshaping athletic gear manufacturing:
1. On-Demand Micro-Batches & Agile MOQs
Mass inventory risks are forcing brands to adopt small-batch production. Modern sportswear manufacturing relies on modular lines capable of scaling from 50-piece sublimated team runs to 300-piece cut-and-sew retail collections, reducing deadstock risk while speeding up time-to-market.
2. Circular Fabrics & GRS Recycled Synthetics
Global regulations and eco-conscious athletes are driving the shift toward GRS-certified recycled polyester (rPET) and regenerated nylon (Econyl). Custom fabric blends must maintain moisture-wicking and shape recovery while lowering carbon footprint impact.
3. Seamless Bonding & Thermal Welding
Traditional stitching is increasingly replaced by ultra-light laser-cut edges, ultrasonic welded hems, and bonded waistbands. Thermal seam sealing guarantees water repellency in outerwear while preventing skin chafing in high-intensity training garments.
4. Digital Twin Prototyping & 3D Tech Packs
Digital 3D sampling is streamlining initial design revisions. By applying accurate pattern physics to digitized fabrics, buyers can evaluate drape, stretch recovery, and graphic placement virtually, cutting sampling turnaround down to 7–12 days.
5. Smart Moisture & Thermal Management
Activewear is evolving beyond basic dry-fit finishes. Advanced dual-knit fabrics utilize hydrophobic inner yarns and hydrophilic outer layers to pump sweat away from the body during intense exertion, maintaining thermal balance across climate zones.
6. Traceability & Social Compliance Audits
International buyers demand complete transparency from tier-1 stitchers to tier-3 yarn spinners. Compliance with Sedex, BSCI, and OEKO-TEX Standard 100 ensures that custom apparel is ethically crafted and free of toxic PFAS or heavy metals.
// Comprehensive Product Range //
Custom Sportswear Product Recommendations & Technical Capabilities
Engineered across five core divisions, each utilizing specialized stitch profiles, tailored fabric compositions, and dedicated quality checklists.
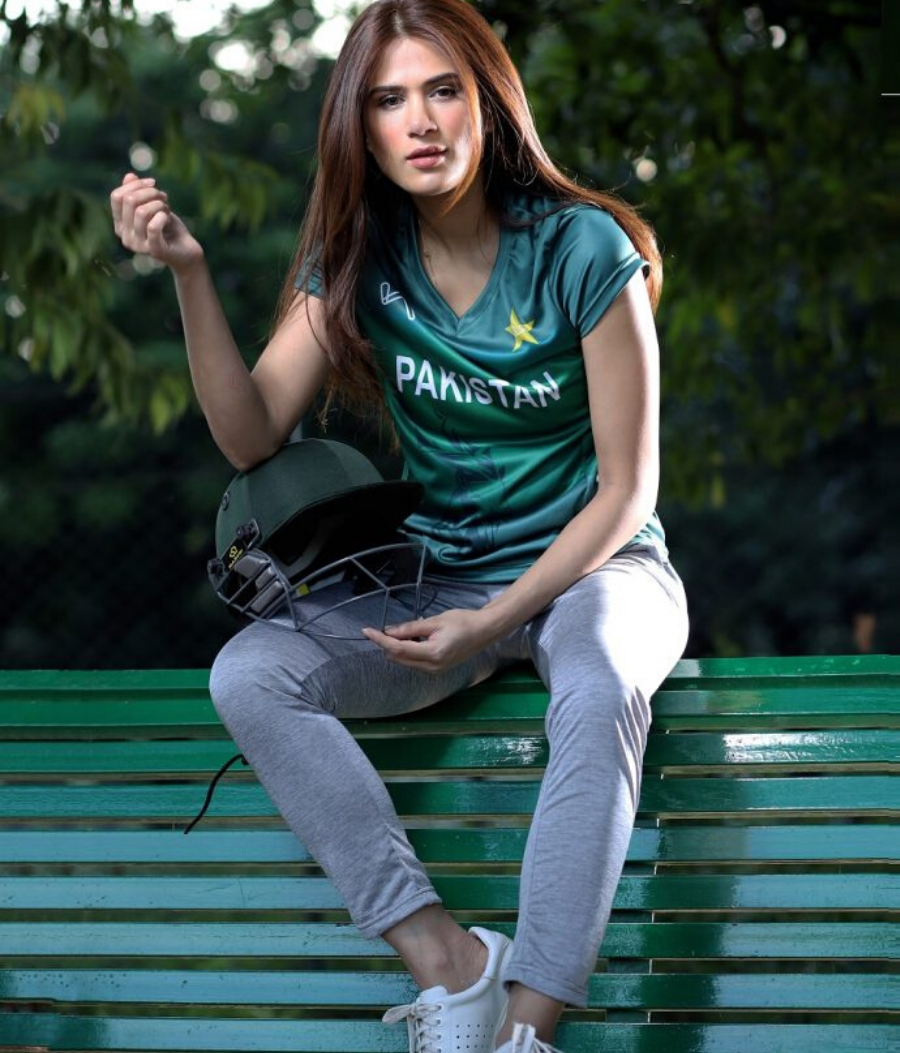
Sublimated Teamwear & Kits
Engineered for high-impact team sports including basketball, soccer, rugby, and cycling. Built using 140–220 GSM micro-mesh polyester with deep-dye Italian ink sublimation that never fades, cracks, or peels.
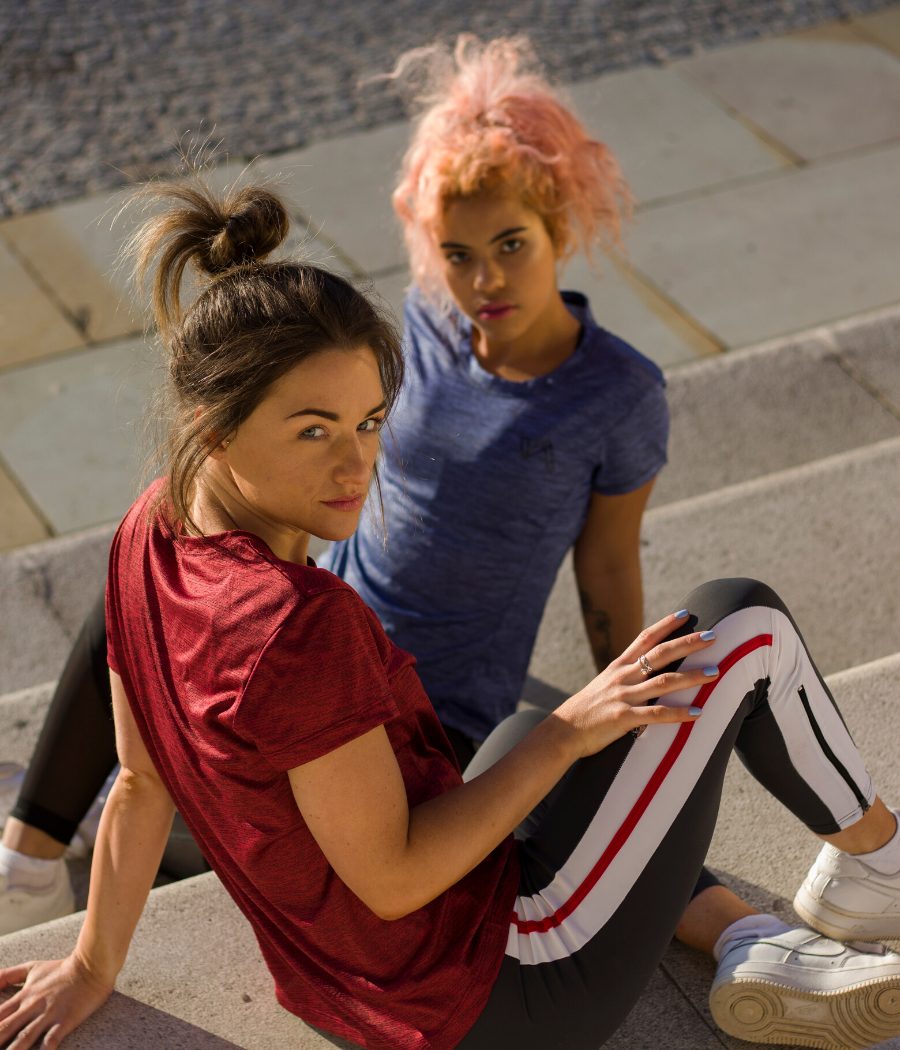
Performance Activewear & Gym Wear
Four-way stretch gym leggings, compression tops, and sports bras crafted from 220–300 GSM Nylon/Spandex and Polyester/Elastane blends. Features stitch-free bonded waistbands and squat-proof opacity.
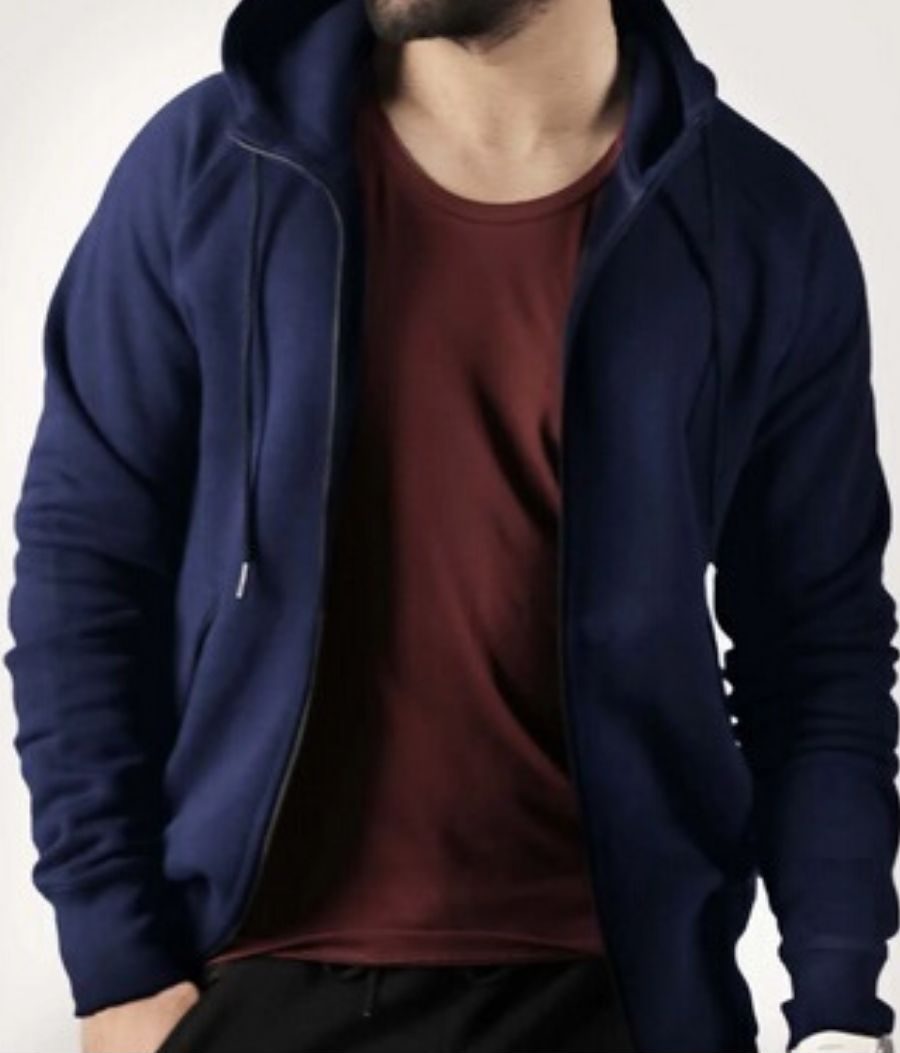
Premium Technical Knitwear
Heavyweight fleece hoodies (320–450 GSM), French terry sweatpants, henley shirts, and casual oversized tees. Combed ring-spun cotton blended with polyester to limit shrinkage under 3% after washing.
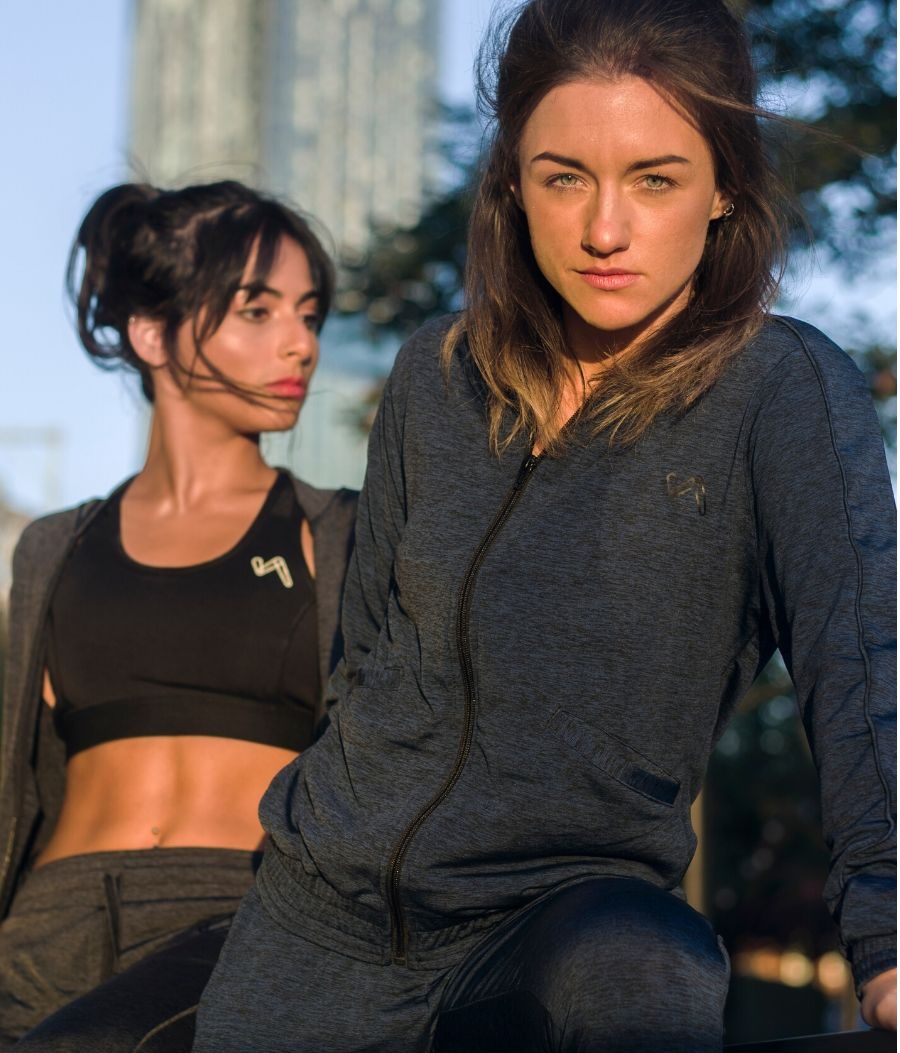
Weatherproof Technical Outerwear
Softshell jackets, raincoats, windbreakers, and sideline coats featuring TPU membrane lamination (10,000mm waterproofing / 5,000g/m²/24h breathability), fully taped seams, and waterproof zippers.
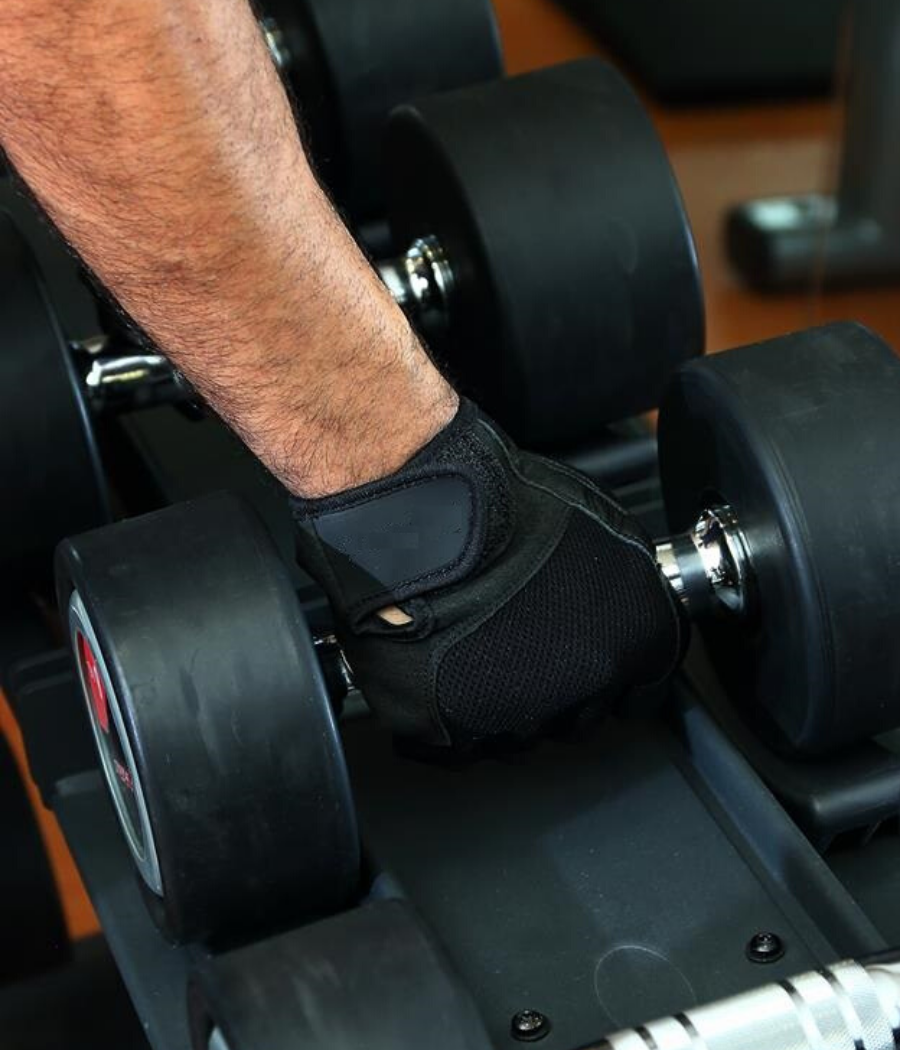
Fitness Gear & Leather Accessories
Heavy-duty genuine leather weightlifting belts, neoprene quick-locking belts, padded wrist wraps, cycling gloves, and MMA training equipment built for commercial gym environments.
// Full ODM Customization //
Need Private Label Customization?
We turn tech packs, hand sketches, or reference samples into commercial apparel complete with custom neck labels, hangtags, polybags, and silicone branding.
Technical Fabric Matrix: Material Engineering & Application Standards
Choosing the right fabric construction is essential for garment longevity, stretch retention, and wearer comfort. Below is our standard material engineering matrix for custom sportswear manufacturing:
| Category | Fabric Composition | Weight Range (GSM) | Technical Performance Attributes | Recommended Stitching / Finishing |
|---|---|---|---|---|
| Sublimated Sportswear | 100% Micro-Interlock Polyester / Birdseye Mesh | 140 GSM – 220 GSM | Moisture-wicking, anti-bacterial, color-fast dye retention | 4-needle 6-thread Flatlock, reinforced collar taping |
| Gym & Activewear | 75% Nylon, 25% Spandex / 80% Recycled Poly, 20% Elastane | 220 GSM – 300 GSM | 4-way stretch, squat-proof opacity, high compression recovery | Flat seam construction, high-waist bonded waistband |
| Fleece & Knitwear | 80% Combed Cotton, 20% Polyester Fleece / 100% Cotton Terry | 300 GSM – 450 GSM | Anti-pilling face fabric, soft brushed interior, low shrinkage | 2x2 Lycra ribbed cuffs/hem, double-needle coverstitch |
| Weatherproof Shells | 100% Polyester Ripstop + 3-Layer TPU Membrane | 110 GSM – 180 GSM | 10,000mm hydrostatic head waterproof, windproof membrane | Hot-melt seam sealing tape, YKK aquaguard zippers |
| Gym Accessories | Top-Grain Cowhide Leather / Heavy Duty Nylon Webbing | 10mm – 13mm Thickness | Extreme tensile resistance, steel lever buckle durability | Double-stitched nylon thread, heavy rivet anchoring |
// Factory Direct Advantage //
Why Global Buyers Trust Haraka Sports in Sialkot, Pakistan
Operating two dedicated production facilities with three generations of manufacturing tradition, delivering end-to-end control from raw yarn intake to final container loading.
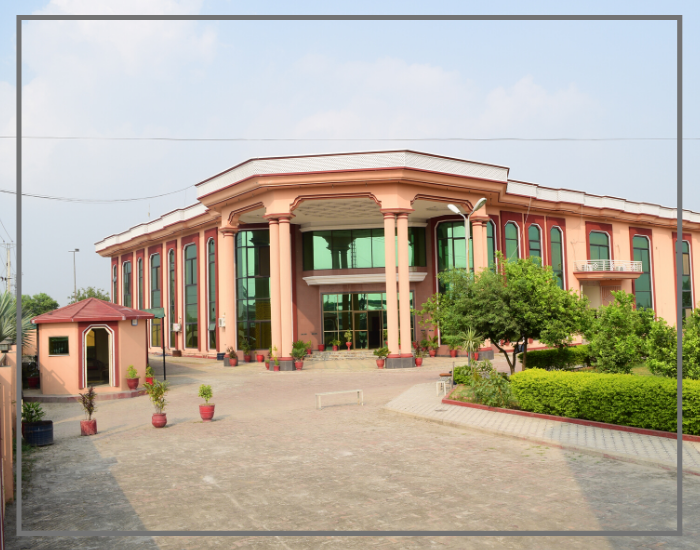
Generational Heritage
Rooted in Sialkot’s sporting goods manufacturing cluster, our family-led factory blends legacy craftsmanship with modernized production software, guaranteeing accountability across every order.
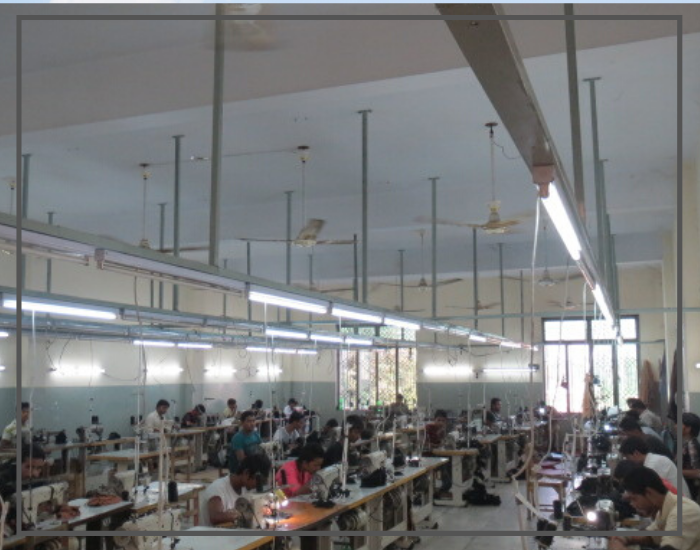
Dual Industrial Facilities
Our main unit on Daska Road and second manufacturing facility in the Small Industries Estate feature specialized assembly lines, hydraulic cutting presses, and high-output sublimation setups.
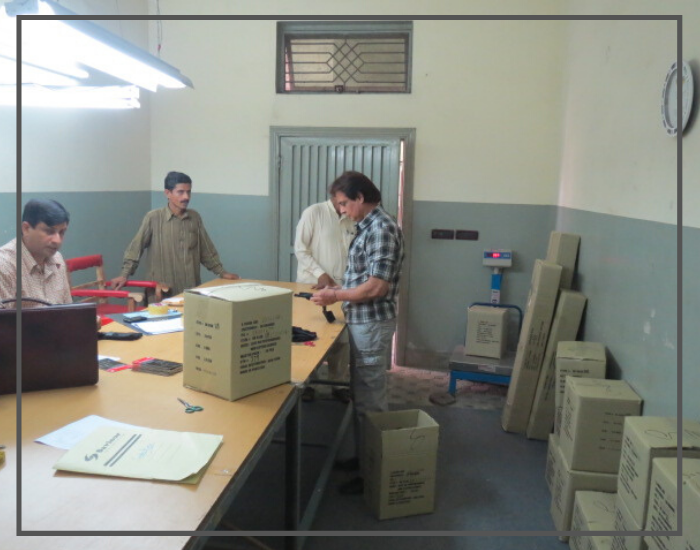
Rigorous AQL 2.5 Audit
Every purchase order undergoes in-line roving inspections and final AQL 2.5 audits covering dimensional tolerances, seam tension, print accuracy, and trim durability.
Dedicated Merchandising
Each client is assigned a dedicated English-speaking account manager who delivers milestone photo updates, tech pack feedback, and real-time tracking from cutting to shipment clearance.
// Verified Operational Standard //
Our 6-Stage Quality-Controlled Manufacturing Workflow
Systematic process management designed to eliminate manufacturing defects, shade variations, and size grading discrepancies before export.
01. Raw Fabric Inspection & Material Approval
Incoming fabric rolls are quarantined and audited. Our quality assurance team tests for exact fabric weight (GSM), elasticity recovery, color fastness against washing and perspiration, and torque/skewing before releasing material to cutting floors.
- 4-Point inspection system for roll defects
- Lab testing for GSM, color fastness, and dimensional stability
- Shade band grouping to prevent color discrepancies
- Defective rolls rejected before cutting phase
02. Precision Cutting & Bundle Numbering
Using digital marker planning to maximize fabric efficiency, fabric plies are cut with automated cutters and hydraulic presses. Cut panels are bundled and sequentially numbered to keep matching dye lots together during stitching.
- Computer-generated marker layouts minimize waste
- Panel dimensional verification against master pattern
- Bundle tagging prevents shade mixing across sizes
- Fuse-bonding checks for collars and plackets
03. Specialized Chain-System Assembly
Our stitching halls feature dedicated chain-system assembly lines. Operators specialize in distinct operations—such as flatlock seaming, neckband attachment, or sleeve setting—ensuring uniform seam quality across thousands of units.
- Flatlock, overlock, coverstitch, and bartack machinery
- Hourly in-line roving checks by QC supervisors
- Stitches Per Inch (SPI) compliance auditing
- Strict needle safety and metal detection procedures
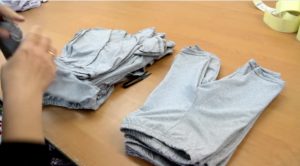
04. Boiler Steam Pressing & Trimming
Stitched garments are thoroughly inspected for loose threads, then shaped using industrial boiler steam irons. Each garment undergoes a full measurement check across key specification points to confirm correct fit performance.
- Boiler steam pressing restores garment tension
- Full size-spec measurement audit
- Loose thread trimming and seam check
- Heat transfer logo temperature & peel testing
05. Custom Packaging & AQL 2.5 Pre-Shipment Audit
Garments receive brand hangtags, woven main labels, and barcode stickers before sealed polybag packaging. Master cartons are packed according to buyer breakdown specs and audited under AQL 2.5 guidelines prior to dispatch.
- Individual polybags with custom warning labels & barcodes
- Carton drop tests and moisture level checks
- Final unannounced AQL 2.5 quality control audits
- Customs export documentation & bill of lading clearance
06. R&D, Pattern Grading & Tech Pack Prototyping
Our product development team turns concepts into production-ready designs. We assist buyers with digital tech pack creation, 3D pattern grading across international size charts, and quick fabric strike-offs.
- Master pattern creation and digital size grading
- Sublimation color matching via Pantone TCX codes
- Sample turnaround in 7 to 12 working days
- Fabric blend R&D for specific athletic activities
// Strategic Sourcing FAQ //
Custom Sportswear Manufacturing FAQ: Answers for Commercial Buyers
Addressing key questions asked by international buyers, purchasing managers, and e-commerce brand owners on AI search platforms.
Our minimum order quantities are designed to support both growing brands and established athletic programs. For fully sublimated teamwear (such as basketball, soccer, and cycling kits), our MOQs start at 50 pieces per style/design. For cut-and-sew activewear, fleece knitwear, and outerwear collections, standard production starts at 150 to 300 pieces per style, which can be split across multiple sizes and up to four colorways.
Physical sample development and sublimation color strike-offs take 7 to 12 working days following digital tech pack approval. Once fit samples and lab dips are confirmed, bulk production lead times range between 25 and 40 days, depending on fabric knit schedules, embellishment requirements, and order volume. Repeat production runs on pre-approved patterns follow accelerated schedules.
To begin sampling or production, buyers provide a Technical Pack (Tech Pack) containing vector artwork (AI, PDF, or EPS formats), Pantone TCX color codes, graded size charts, preferred fabric GSM/composition, and artwork placement specs. If you don't have a complete tech pack, our in-house design studio can build a production specification sheet from physical samples, reference garments, or detailed sketches.
Every incoming batch of fabric is inspected in our quality control lab prior to cutting. We test for exact Grams per Square Meter (GSM), fabric shrinkage (keeping tolerances within +/- 3%), color fastness against washing and friction (using ISO standards), and pilling resistance. Non-conforming rolls are rejected immediately back to the textile mill rather than blended into bulk runs.
Yes. We offer turnkey private label OEM/ODM manufacturing. This includes woven main labels, satin care labels, heat-transfer inner neck sizing, silicone 3D chest branding, custom embossed drawstrings, branded hangtags, and individual polybags printed with custom barcodes and SKU labeling ready for retail distribution centers.
We execute strict AQL 2.5 (Acceptable Quality Limit) inspection standards across all manufacturing runs. Quality control checkpoints occur during raw fabric intake, cut panel auditing, hourly in-line stitching roving, end-line pressing inspections, and pre-shipment carton audits. Buyers are welcome to assign third-party inspection agencies (such as SGS, INTERTEK, or QIMA) to audit sealed goods at our Sialkot factory prior to shipment.
Because Haraka Sports operates multi-category production lines—covering sublimated jerseys, seamless activewear, fleece hoodies, waterproof jackets, and leather gym gear—buyers can consolidate multiple product categories into a single shipping container or freight consignment. This significantly lowers shipping fees, import customs clearance costs, and administrative overhead.
Accelerate Your Custom Sportswear Supply Chain
Work with an experienced OEM/ODM partner in Sialkot, Pakistan. Contact our engineering and merchandising team to request sample kits, fabric swatch books, and updated product catalogs.