Sourcing Architecture: Technical Compliance & Regulatory Alignment for US Importers
The North American athletic apparel landscape is currently undergoing a structural pivot. Sourcing directors, commercial gym chains, and direct-to-consumer (D2C) private labels across the United States can no longer rely solely on aesthetic design; apparel performance is now measured by rigorous physical data, chemical compliance, and verifiable supply chain integrity. As a certified OEM/ODM apparel factory operating with dual production facilities in Sialkot, Pakistan, Haraka Sports bridges the gap between global industrial manufacturing capacity and US regulatory standards.
Information Gain Metric: Why CE Certification Matters in the US Market. While CE marking is historically rooted in European safety directives, US buyers increasingly utilize European EN standards (such as EN 13758-1 for UPF solar protection and EN ISO 6330 for domestic wash durability) as benchmark proof of high-tier textile compliance, non-toxic dye profiles, and mechanical safety.
1. Advanced Material Science: Fabric GSM, Yarn Densities & Moisture Dynamics
High-intensity gym tank tops and athletic apparel undergo extreme mechanical tension, sweat contact, and repeated wash cycles. Standard retail apparel often fails under commercial conditions due to seam slippage or fabric pilling. Our factory utilizes engineered poly-elastane, high-tenacity nylon-spandex, and combed ring-spun cotton blends meticulously weighted from 140 GSM (featherweight marathon singlets) to 300 GSM (sculpting compression activewear).
Key technical benchmarks executed in our production lines include:
- Capillary Action Moisture Vapor Transmission Rate (MVTR): Achieving over 8,000 g/m²/24hr to ensure immediate sweat dispersion during intense cross-training and bodybuilding workouts.
- Four-Needle Six-Thread Flatlock Seaming: Utilizing high-stretch elastic filaments that lie flush against the skin, eliminating friction points and delivering seam strength up to 35 lbs of lateral tension.
- Colorfastness & Pilling Ratings: Tested to Grade 4-5 under ISO 105-B02 (Light Fastness) and ISO 12945-2 (Martindale Abrasion), ensuring vibrant sublimation print retention and zero surface fuzzing after 50+ commercial wash tests.
2. Chemical Safety & OEKO-TEX Standard 100 Compliance
Under the US Consumer Product Safety Improvement Act (CPSIA) and California Proposition 65 regulations, imported textiles must strictly limit heavy metals, phthalates, and banned azo dyes. Our manufacturing workflow enforces zero-tolerance chemical screening on all raw knitted fabrics, sublimation inks (utilizing Japanese Epson UltraChrome HD inks), and heat-transfer trim items prior to cutting.
1. HIIT & CrossFit Box Gym Apparel
Built for extreme friction against barbells and plyo boxes. Reinforced drop-armhole tank tops and high-durability singlets engineered with abrasion-resistant poly-spandex blends that withstand intense friction without fraying.
2. Commercial Gym Chains & Merchandise
Private label programs for regional and national gym franchises (e.g., Gold's, Equinox, F45 suppliers). High-volume, standardized sizing algorithms customized to US specs with custom woven neck labels and polybag barcoding.
3. Collegiate Athletics & Varsity Clubs
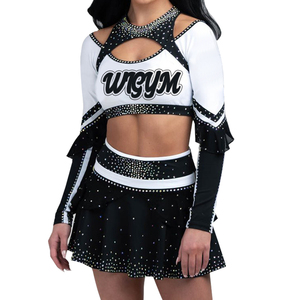
NCAA-compliant teamwear singlets and training tops utilizing color-locked dye sublimation. Ensures exact pantone matching for university logos and resistance to heavy sweat during intensive multi-season training.
4. Athleisure Retail & Amazon FBA Brands
Retail-ready turn-key apparel development. From custom silicon gel logo applications to custom branded hangtags and pre-sorted size packs ready for direct fulfillment into US Amazon distribution centers.
5. Bodybuilding & Physique Expos
Deep scoop-neck stringer tanks and tapered-fit muscle tees designed to accentuate physique proportions. Crafted with micro-modal and elastane mixes for ultra-soft drape and stretch recovery.
6. Tactical & Outdoor Fitness Apparel
Heavy-duty, UPF 50+ sun protection hooded activewear designed for outdoor boot camps, trail running, and high-exposure outdoor training across sunny US states such as Florida, Texas, and California.
Key Localized Trends Driving the US Gym Tank Top & Activewear Market
Understanding user intent and purchasing habits in the United States requires analyzing the technological and lifestyle macro-shifts occurring across North America. Buyers are shifting away from traditional low-cost commodity sourcing toward high-value, sustainable, and specialized functional apparel.
Trend A: The Surge in Recycled Synthetics & Circular Textiles (rPET)
Environmental responsibility is no longer optional for US apparel importers. American consumers actively look for GRS (Global Recycled Standard) labels on activewear. Our production lines feature recycled polyester derived from post-consumer plastic bottles, offering identical tensile strength, moisture-wicking capability, and hand-feel while reducing carbon footprint during yarn extrusion by up to 45% compared to virgin synthetics.
Trend B: Seamless 3D Knitting Technology vs. Traditional Cut-and-Sew
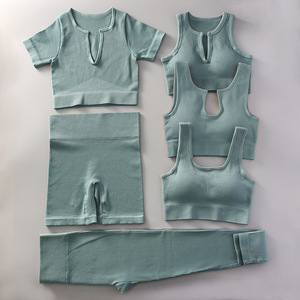
Seamless activewear represents one of the fastest-growing market segments in the US. By utilizing specialized circular knitting machinery, we produce gym tank tops and bra sets that feature targeted ventilation zones engineered directly into the structure of the garment—eliminating unnecessary seams, reducing material scrap waste, and delivering second-skin comfort.
Trend C: Micro-Batch Customization & Agility in Private Label Inventory
With US brands attempting to mitigate supply chain bottlenecks and high warehousing costs, the era of massive 10,000-piece single-style MOQs is dwindling. Importers require agile OEM manufacturing that allows low initial development runs (from 150-300 pieces per cut-and-sew style) followed by rapid bulk scaling upon market testing validation.
Factory Expertise: Why Haraka Sports is the Benchmark Supplier
Founded as a third-generation family manufacturing enterprise in Sialkot, Pakistan—the world's historic hub for sporting goods and technical textile manufacturing—Haraka Sports brings decades of hands-on expertise directly to American B2B buyers.
Dual Production Facilities
Operating two modern units (Main Factory on 8 km Daska Road and Unit 2 in Small Industries Estate, Sialkot), allowing complete separation between high-volume knitted sportswear and specialized technical equipment/accessories.
6-Stage Documented QC Workflow
Every purchase order follows an audited track: 1. Incoming Fabric GSM & Shrinkage Testing, 2. Marker & Hydraulic Cutting Audit, 3. Chain-System Line Inspection, 4. Steam Pressing & Trimming, 5. Pre-Shipment AQL 2.5 Sampling, 6. Final Barcode & Packaging Verification.
Full OEM/ODM Private Label Services
Our in-house R&D room transforms tech packs or rough mood boards into graded master patterns within 7 to 12 working days, complete with customized heat-transfer neck labels, silicone printing, and custom hangtag executions.
Factory Transparency Guarantee: Sourcing managers are invited to review production photo logs at every critical stage—fabric arrival, panel cutting, line stitching, and carton sealing. We welcome third-party international inspection agencies (such as SGS, INTERTEK, or Bureau Veritas) to our Sialkot facility prior to balance payment release.
What are the typical Minimum Order Quantities (MOQs) for US custom orders?
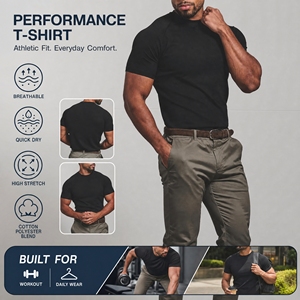
For dye-sublimated gym tanks and teamwear, our development MOQ starts as low as 50 pieces per design. For custom cut-and-sew apparel, seamless activewear, and muscle fit t-shirts, standard production runs typically start at 150 to 300 pieces per style, which can be split across standard US size gradings (XS through 3XL) and up to 4 custom colorways.
How long does sample development and bulk shipping take to the United States?
Fit samples and sublimation strike-offs are completed and dispatched within 7 to 12 working days post tech pack confirmation. Bulk production lead times average 25 to 40 days depending on fabric availability and embellishment requirements. Express air freight to US destinations (via DHL/FedEx) takes 4 to 7 days, while ocean freight to US West/East Coast ports averages 25 to 35 days.
Does Haraka Sports assist with US Customs, Tariff HTS Classification, and Duty compliance?
Yes. We provide complete commercial invoice documentation, packing lists, and correct HTS Code classification (such as HTS 6109.90 for synthetic knitted tanks/tees). We work seamlessly with your nominated US customs broker or offer Delivered Duty Paid (DDP) shipping directly to your warehouse door.
How do you ensure sizing consistency tailored specifically for North American fit standards?
We do not use generic Asian sizing charts. Our pattern-making department utilizes standardized US & European measurement specs. We provide full digital CAD grading tables prior to sample production, allowing you to approve key dimensions including chest drop, shoulder seam angle, torso length, and armhole circumference.
Can multiple activewear products and gym accessories be consolidated into a single shipment?
Absolutely. Because we manufacture custom apparel (tank tops, hoodies, shorts, leggings) alongside leather & nylon gym equipment (lifting belts, straps, gloves) across our Sialkot production units, we consolidate your entire purchase order into unified export containers—significantly reducing logistics overhead for US buyers.