CE Certified Rugby Shirts Manufacturers & Factories for London
Engineering Heavy-Contact Technical Athletic Wear & OEM/ODM Supply Chains for Greater London Clubs, Universities & Wholesale Brands
Recommended High-Performance Athletic Lines
Custom OEM/ODM manufacturing solutions engineered for athletic durability, high tensile strength, and quick-dry moisture management.
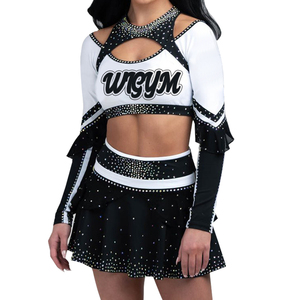
Custom All Star Performance Team Wear Apparel
Heavy-duty elastane-blended construction featuring reinforced stress-point stitching, high elasticity, and customizable performance accents for elite athletic teams.
1. Executive Sourcing Guide: CE Certification & Safety Compliance for London Rugby Procurement
Sourcing rugby jerseys for clubs across Greater London, the Home Counties, and the broader UK market requires an understanding of rigorous European and UK regulatory standards. Modern rugby apparel is no longer classified merely as leisure fashion; under British and European safety paradigms, contact-sport uniforms operate as high-performance protective textiles.
The CE Marking (Conformité Européenne) and its post-Brexit UK counterpart, the UKCA (UK Conformity Assessed) mark, certify that garment factories adhere to strict health, safety, and environmental protection benchmarks. When procuring technical rugby kits for London RFCs (spanning RFU National League clubs down to grassroots university BUCS teams), procurement directors must verify specific technical compliance vectors:
Compliance Standard
Technical Parameter Tested
Performance Standard Required
Relevance to London Buyer Risk Mitigation
BS EN 13758-2 / CE UPF
Solar Ultraviolet Protective Properties
UPF 50+ blocking >98% harmful UVA/UVB rays
Protects players during early-season and summer 7s tournaments across the UK.
Eliminates mid-match jersey tearing, seam slippage, and neck-line collar snapping during scrums and tackles.
OEKO-TEX Standard 100 Class I
Chemical Hazard & Toxicity Audit
Zero banned azo dyes, formaldehyde, or heavy metals
Guarantees non-allergenic skin contact under conditions of intense sweating and chafing.
UK REACH Regulation
Substance of Very High Concern (SVHC)
Full compliance with UK import chemical thresholds
Prevents customs impoundment at UK entry ports (London Gateway, Dover, Heathrow freight hubs).
As a third-generation factory based in Sialkot, Pakistan—the globally recognized epicenter of sporting goods manufacturing—our manufacturing lines integrate automated yarn-stress verification, heavy-duty interlock poly-elastane knits, and eco-compliant dispersion dyes designed specifically to pass UK import audits.
2. Technical Evolution: Heavyweight Traditional Cotton vs. CE-Certified Sublimated Poly-Elastane
London’s unique micro-climate—characterized by damp, rain-soaked autumn pitches and cold winter matchdays—places extreme performance demands on matchday kits. Traditional 100% heavy cotton jerseys (380-450 GSM), while historically revered, absorb up to 250% of their weight in surface moisture and mud. This dramatically increases player fatigue, restricts upper-torso mobility, and exacerbates seam bursting under scrums.
Our factory engineered the next generation of CE-Certified 300-340 GSM High-Tenacity Technical Polyester Interlock. Through a proprietary blend of 88% micro-denier polyester and 12% high-recovery elastane, we provide an anti-grab, moisture-wicking structure that maintains ultra-low wet weight retention.
Traditional Cotton Rugby Shirts
High water absorption rate (>200% dry mass).
Prone to shrinkage (5-8% after industrial wash).
Collar tearing under dynamic neck-grab forces.
Screen-printed logos crack and peel after one season.
Heavy thermal retention leads to overheating.
CE Technical Sublimated Rugby Shirts
Hydrophobic capillary action wicks sweat in <3 seconds.
Dimensional stability: <1% shrinkage post-wash.
Reinforced double-bound Loop-21 ergonomic collar.
Full-bleed sublimation: Zero weight addition, lifetime color fastness.
Multi-channel micro-ventilation panels for temperature control.
3. Localized Application Scenarios: Serving the Greater London Rugby Ecosystem
Rugby in London operates across diverse competitive tiers—each presenting distinct performance requirements, aesthetic traditions, and commercial budgets. Our custom OEM/ODM factory lines cater directly to these distinct localized buying segments:
A. RFU Championship & National League Clubs
Semi-professional and professional outfits (e.g., clubs in Richmond, Barnes, Blackheath, and Rosslyn Park) demand hyper-fitted, body-mapping silhouettes with built-in GPS tracker pockets between the shoulder blades. Our factory constructs custom 340 GSM tear-resistant spandex-polyester panels with flatlock structural seams to withstand professional tackles.
B. University BUCS Leagues & Medical Schools
London university athletic unions (Imperial College, King's College London, UCL, Brunel) require vibrant, multi-sponsor sublimated match kits and matching off-field outerwear. We offer integrated club bundles (Match Jersey, Shorts, Socks, Tracksuits, and Hoodies) with low minimum order quantities (MOQs) starting at just 50 units.
C. Corporate & City Finance Tournaments
Annual charity tournaments and financial sector leagues in Canary Wharf and the City of London mandate high-end classic cut retro rugby shirts mixed with modern performance fabrics. We offer custom embroidery, gold/silver wire bullion crests, and premium woven button plackets.
D. Youth Academies & School Sports Trust Kits
Grassroots youth programs require strict safety compliance—specifically soft-touch rubber buttons (preventing facial lacerations during contact) and non-toxic OEKO-TEX certified fabrics. Our youth kits conform fully to British RFU safety directives for age-grade rugby.
4. Macro Trends Shaping Rugby Shirt Procurement in London (2025-2030)
Procurement heads and sportswear brand directors in London are updating their supply chain requirements to reflect three dominant market shifts:
01
GRS Recycled Poly Fibers
UK sustainability mandates mean top-tier clubs favor Global Recycled Standard (GRS) certified yarn made from ocean-bound PET bottles without compromising tear strength.
02
GPS & Telemetry Pockets
Modern coaching requires performance data. Seamless internal neoprene pockets are now standard for housing GPS performance monitoring units during matches.
03
Anti-Grab Ergonomic Fits
Traditional loose fits are replaced by tight, skin-second contours. Sublimated elastane side panels make it nearly impossible for opposition defenders to grab leverage.
5. Factory Excellence: Our 6-Stage ISO Quality Control Workflow
Operating out of two specialized production facilities in Sialkot (Daska Road & Small Industries Estate), our 3rd-generation family-owned factory eliminates third-party intermediary markups while enforcing rigorous quality checkpoints on every order.
Stage 1
Fabric Inspection & GSM Testing
Incoming fabric rolls undergo lab inspection for GSM consistency, color fastness to perspiration/rubbing, and dimensional shrinkage under high-temperature washing.
Stage 2
CAD Pattern Grading & Hydraulic Cutting
Digital tech packs are converted to automated marker plans. Panels are cut via hydraulic precision presses to ensure zero measurement variances across sizes S to 5XL.
Stage 3
HD Sublimation & Embroidery
Italian Kian sublimation inks are heat-fused into the polyester core at 210°C, ensuring logos, club crests, and pantone colors never fade, peel, or add garment weight.
Stage 4
Specialized Chain-System Stitching
Panels move through dedicated lines equipped with 4-needle 6-thread flatlock machines, heavy-duty bar-tackers for collar joints, and reinforced hem cover-stitchers.
Stage 5
Boiler Steam Audit & Trimming
Garments undergo boiler steam pressing to lock shape, followed by 100% manual thread trimming, loose end inspection, and dimensional spec verification.
Stage 6
AQL 2.5 Pre-Shipment Inspection
Independent internal auditors execute final sampling under AQL 2.5 standards before goods are individually polybagged, barcoded, and packed into heavy-duty export master cartons.
6. Frequently Asked Questions by London Sportswear Buyers & Club Merchandisers
Q1: How do you verify CE and UKCA compliance for UK-bound shipments?
Every bulk production lot is accompanied by a Factory Certificate of Conformance (CoC), validating fabric tensile strength (ISO 13934-1), chemical safety (REACH Annex XVII), and color fastness. Lab test reports from accredited bodies (Intertek/SGS) can be commissioned upon request.
Q2: What is the lead time for door-to-door air freight delivery into London?
Fit samples and sublimation strike-off proofs take 7-10 working days. Upon sample approval, bulk manufacturing requires 20-30 days. Express air freight via DHL/FedEx reaches London freight centers (LHR) within 4-6 business days.
Q3: What are your Minimum Order Quantities (MOQs) for custom teamwear?
For fully sublimated match kits (Jerseys and Shorts), our MOQ starts at only 50 pieces per style, which can be split across player sizes. For larger custom cut-and-sew apparel lines (such as fleece hoodies or sideline jackets), MOQs start at 150-300 pieces.
Q4: Can you handle private label branding, custom packaging, and EORI paperwork?
Yes. We offer complete OEM/ODM private label execution: custom woven neck labels, heat-transfer size logos, custom hangtags, branded polybags, and pre-sorted team pack distribution. We provide full commercial invoices and HS-code documentation to streamline your UK Customs import clearance.
Partner with Sialkot's Premier Rugby Apparel Manufacturer
Elevate your club or brand’s matchwear with CE-certified quality, direct factory pricing, and technical fabric innovation tailored for the UK market.