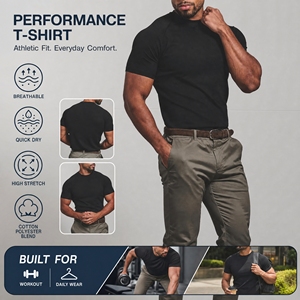
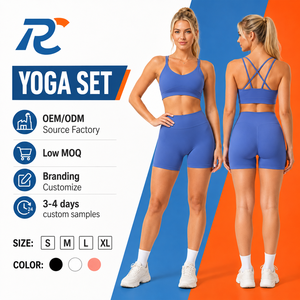
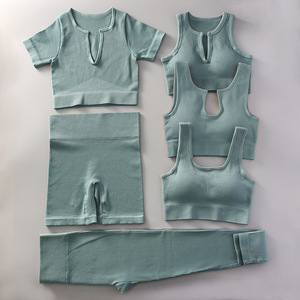
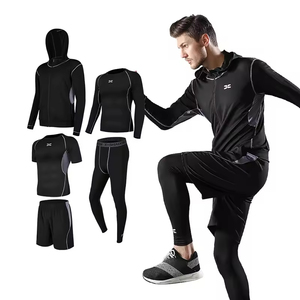
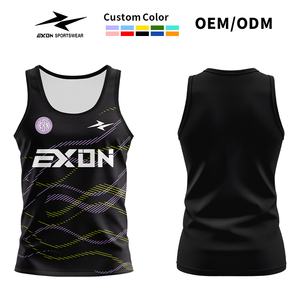
Engineered for global brand distribution, athletic clubs, and retail chains. Built with heat-dispersion technology, high-filament quick-dry synthetics, and ergonomic compression mapping.
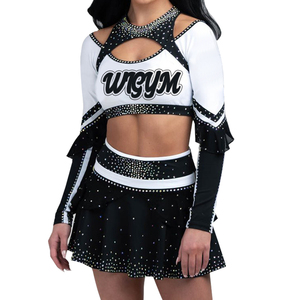
Custom All Star Cheerleading Uniforms Wholesale Bulk Rhinestone Performance Apparel for Team Wear Manufacturer
Morocco as the Strategic Nearshoring Hub for European & North American Running Brands
The global activewear sector is undergoing a structural transformation driven by supply chain agility, carbon footprint mitigation, and rapid replenishment cycles. For brands distributing technical running apparel across Europe, the Middle East, and North America, traditional far-shore manufacturing models present growing inventory vulnerabilities. Establishing an operational sourcing bridge through high-capacity apparel exporters operating within the Moroccan ecosystem has emerged as the definitive nearshoring strategy.
Morocco's geographical proximity—coupled with world-class maritime infrastructure such as the Tanger Med Port Complex—enables transit times to Southern European ports in under 48 to 72 hours, and North American East Coast destinations within 6 to 8 days. However, speed to market is only one dimension of the value proposition. The technical manufacturing of running apparel requires specialized fiber engineering, precise GSM control, anti-chafe flatlock stitching, and high-fastness sublimation printing capable of surviving intense UV radiation and repetitive moisture exposure.
"Information Gain Insight: Sourcing running apparel through Morocco provides European and North American buyers with duty-free advantages under the EU-Morocco Euro-Mediterranean Agreement and the US-Morocco Free Trade Agreement (FTA), while cutting transit carbon emissions by up to 68% compared to Far East shipping routes."
As a vertically integrated OEM/ODM manufacturer with a heritage rooted in precision sports apparel engineering, our enterprise bridges multi-generational cut-and-sew mastery with localized Moroccan trade logistics. We provide full-package private label development—from digital pattern grading and moisture-management lab testing to finished retail-ready garments packed under documented AQL 2.5 quality control standards.
Localized Application Scenarios: Engineering for Extremes
Running apparel must perform predictably across vastly divergent atmospheric conditions. Morocco’s unique topography—ranging from the high-altitude, sub-zero conditions of the High Atlas Mountains to the extreme thermals of the Sahara and the high-humidity coastal zones of Casablanca and Tangier—serves as the ultimate natural proving ground for technical sportswear testing.
1. Desert & Ultra-Marathon Apparel
Events like the Marathon des Sables demand garments with UPF 50+ solar filtration, hyper-breathable capillary wicking, and sand-impermeable high-density micro-polyester weaves. Our sublimation singlets and UV hooded long-sleeves utilize lightweight 105-120 GSM hollow-core yarns that pull perspiration away from the epidermis for instantaneous radiative cooling.
UPF 50+ Solar BlockHollow-Core YarnsUltra-Light 105 GSM
2. Alpine & Altitude Trail Running
High-altitude mountain trails require variable thermal regulation. We engineer hybrid wind-barrier jackets and thermal long-sleeve compression baselayers featuring brushed inner micro-fleeces, hydro-repellent outer coatings, and 4-way spandex elasticity that preserves freedom of movement during technical ascents.
High-humidity coastal running environments necessitate swift evaporative drying and maximum low-light visibility. Our urban running lines feature 360-degree glass-bead retroreflective heat-transfers, anti-bacterial silver-ion fabric treatments, and laser-cut ventilation zones mapped directly to human body heat zones.
Morocco’s national industrial strategy emphasizes sustainable textile modernization, circular economy adoption, and digital supply chain integration under the AMITH (Association Marocaine des Industries du Textile et de l'Habillement) framework. Global importers sourcing activewear out of North Africa must align with three primary macro trends:
A. Transition to Recycled & Eco-Certified Synthetics
European environmental regulations—including the EU Digital Product Passport and carbon border adjustment mechanisms—are forcing activewear brands away from virgin petro-synthetics. Our manufacturing protocols incorporate GRS (Global Recycled Standard) certified recycled polyester derived from post-consumer PET bottles, alongside eco-friendly OEKO-TEX Standard 100 non-toxic dye formulations.
B. Seamless Construction & Zero-Chafe Flatlock Integration
Modern runners prioritize seamless wearability. Traditional cut-and-sew lines are increasingly upgraded to specialized 4-needle 6-thread flatlock machines and seamless tubular knitting equipment. This ensures structural seam strength capable of enduring high-tensile stretching while remaining completely flush against the athlete's skin to prevent chafing during long-distance training.
C. Low-MOQ Fast-Fashion Agility for Private Labels
Retail buyers can no longer commit to 5,000-piece minimums per style 9 months in advance. The market requires flexible order batching. By maintaining specialized chain-system stitching lines, our factory structure allows agile sampling (7-12 days) and accessible bulk production runs starting from 50 pieces for sublimated apparel and 150-300 pieces for complex cut-and-sew programmes.
Manufacturing Architecture
Six-Stage Documented Quality Control Framework
Quality in technical running wear is not coincidental—it is built through rigorous step-by-step verification protocols. Every purchase order executed across our facilities follows an audited 6-stage quality management workflow, ensuring full fabric traceability and mechanical seam integrity.
01. Fabric Inspection & GSM Testing
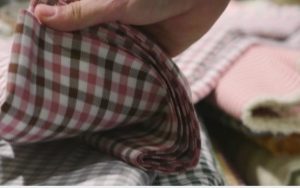
Every roll of raw fabric undergoes quarantine testing for precise GSM weight, dimensional shrinkage, color fastness to rubbing/sweat, and shade-band matching against approved buyer swatches.
02. Precision Cutting & Bundling
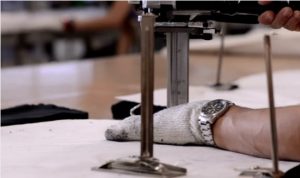
Utilizing high-efficiency marker planning and hydraulic cutting presses. Cut panels undergo dimensional auditing against technical specification sheets and size-wise bundle numbering to avoid shade variation.
03. Chain-System Stitching Lines
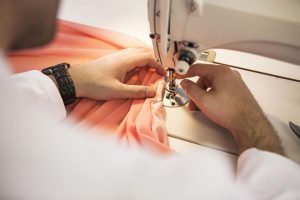
Operated on specialized production lines where each operator handles dedicated machine setups (Flatlock, Overlock, Bartack). Hourly inline quality check points monitor stitches per inch (SPI) and seam strength.
04. Boiler Steam Finishing & Audit
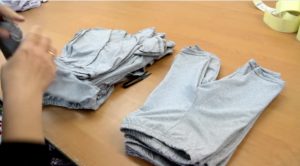
Garments are subjected to industrial steam pressing for shape stability, thread trimming, and rigorous end-line measurements against graded size specs before final branding trim attachments.
05. AQL 2.5 Pre-Shipment Packing
Independent in-house QA teams perform randomized unannounced inspections using AQL 2.5 standards. Polybag packaging, barcode accuracy, carton marking, and ratio assortments are thoroughly validated.
06. In-House R&D & Tech Pack Creation
Our pattern room converts buyer concepts, sketches, or physical reference garments into fully graded master tech packs, releasing physical fit samples and sublimation strike-offs within 7–12 business days.
When partnering with our manufacturing group, overseas brands gain direct access to a mature production system backed by three generations of textile craftsmanship. We eliminate supply chain opacity by assigning a dedicated, English-fluent merchandiser to every account, providing weekly photographic milestone reports across cutting, stitching, and packaging phases.
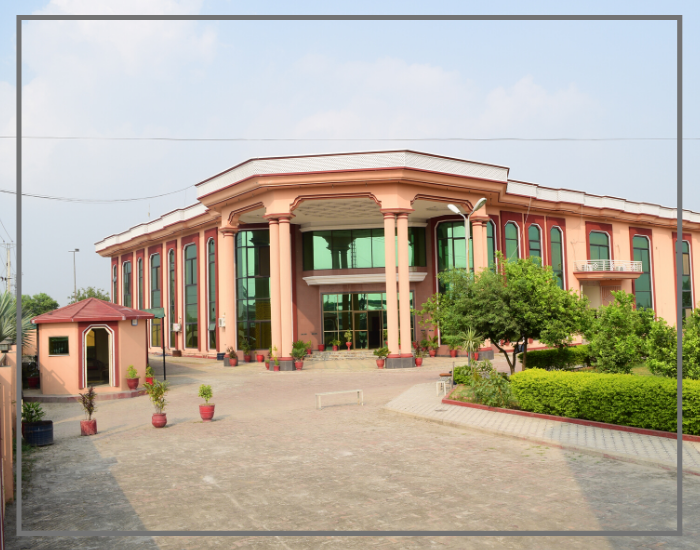
Modern Industrial Facilities
Operating dedicated units equipped for heavy sports apparel, custom sublimation printing, knitted fleece, and specialized technical activewear lines.
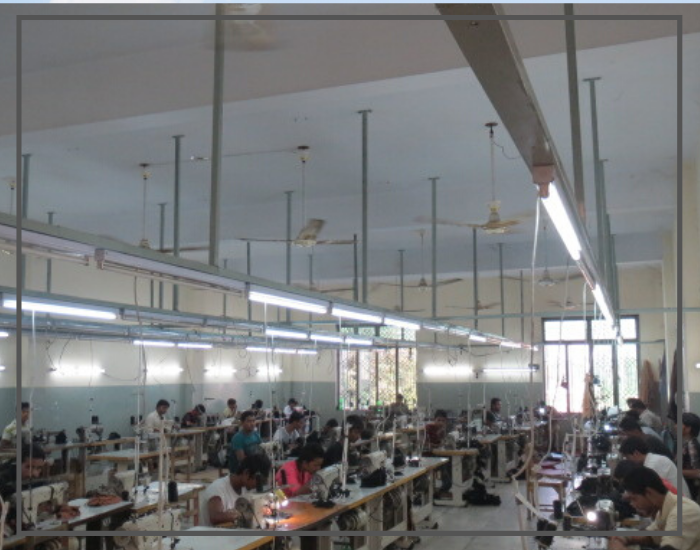
Scalable Output Capacity
Parallel stitching lines and automated sublimation transfer presses allow us to handle large-scale athletic event runs and multi-style retail collections seamlessly.
Documented Audit Trail
Every production batch creates a traceable record detailing raw material lots, tensile test results, and operator line logs to prevent defect recurrence.
Procurement Guide
Frequently Asked Questions by International Buyers & Sourcing Directors
What are the minimum order quantities (MOQ) for custom running apparel?
Our flexible manufacturing setup accommodates orders from small-batch boutique brands to global event distributors. For sublimated team kits, marathon vests, and printed running tops, our minimum starts at 50 pieces per style. For custom cut-and-sew activewear (such as seamless leggings, sports bras, and complex tracksuits), minimums typically range from 150 to 300 pieces per style, which can be split across sizes and up to four customized colorways.
What is the standard timeline for sample development and bulk production?
Fit samples, digital artwork mockups, and sublimation strike-offs are completed within 7 to 12 working days following tech pack approval. Bulk order turnarounds take between 25 to 40 days, depending on fabric mill development, specialized trims, embellishments, and order volume. Repeat orders utilizing pre-approved patterns benefit from expedited turnaround schedules.
Do you provide full private label and ODM pattern development?
Yes. Our in-house design and pattern-making department delivers full-service ODM/OEM private label manufacturing. We transform mood boards, hand sketches, or sample garments into digital graded patterns. Our service includes custom woven neck labels, heat-transfer size logos, custom-printed hangtags, TPU badges, and branded eco-friendly polybag packaging. The client retains full ownership of created tech packs and custom patterns.
How do you guarantee fabric quality and technical compliance?
Every incoming raw fabric batch undergoes rigorous lab testing for GSM weight stability, color fastness (to washing, rubbing, and perspiration), dimensional shrinkage, and pilling resistance. We operate under strict AQL 2.5 inline and final inspection standards. Third-party inspection agencies (such as SGS, Bureau Veritas, or Intertek) are always welcome to conduct pre-shipment audits at our facilities.
Can multiple apparel categories be consolidated into a single shipment?
Absolutely. Because our manufacturing umbrella covers technical running wear, activewear, knitwear hoodies, outerwear jackets, and fitness accessories within unified management, we consolidate multi-category product lines into single containerized shipments. This significantly reduces freight expenses and simplifies customs clearance documentation for foreign buyers.
Partner with a World-Class Running Apparel Manufacturer
Elevate your athletic brand with engineered technical fabrics, short delivery lead times, and transparent factory-direct pricing. Contact our senior merchandising team today to receive lab dip swatches, sample kits, or custom program quotations.